

Cutting, Bending & Forming Solutions
Sheet Metal Fabrication Machines
Sheet metal machinery for cutting, punching, bending, rolling and forming, selected according to the material, thickness, part geometry, required quality and production target.
Types in this category
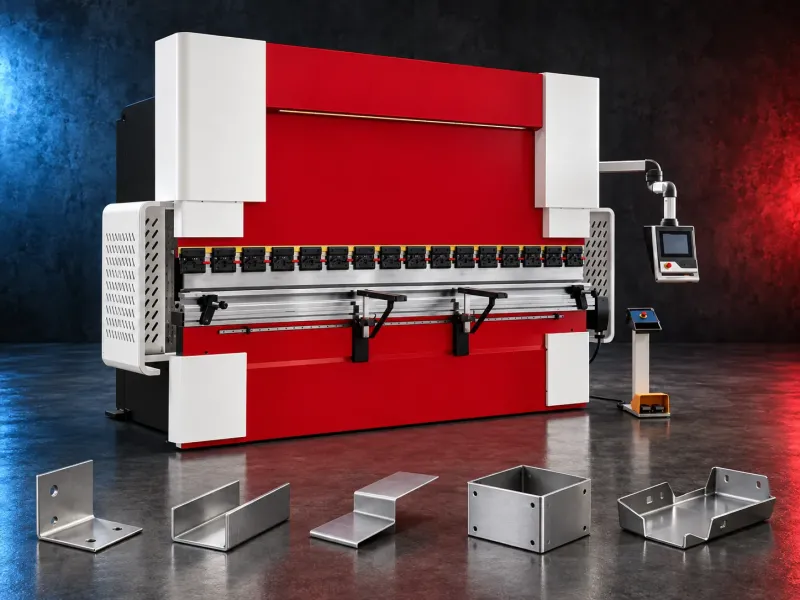 CNC Hydraulic Press BrakeCNC-controlled hydraulic press brakes for bending sheet metal components according to defined angles, dimensions and production requirements.
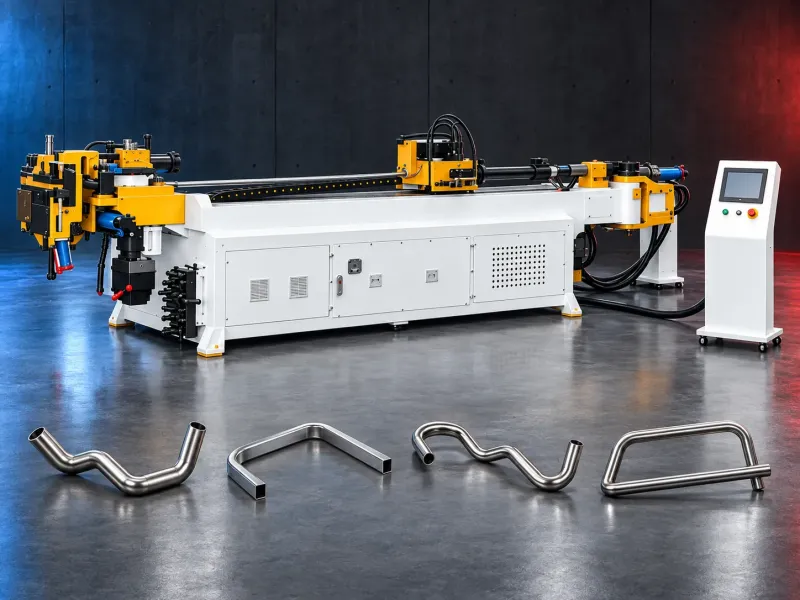 CNC TUBE BENDING MACHINECNC tube bending machines control the bending sequence to produce defined tube and pipe geometries. Selection depends on the material, section, diameter, wall thickness, bend radius, part geometry, accuracy, and production volume.
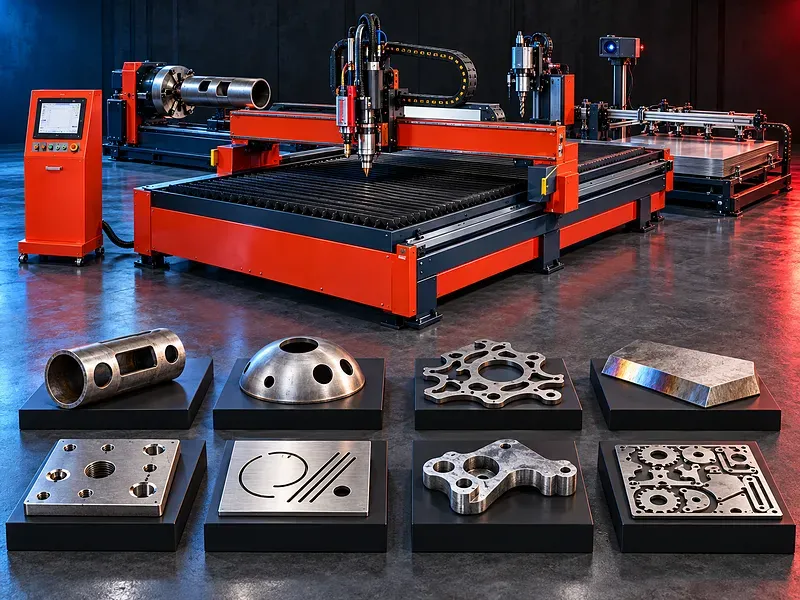 CNC Gantry Plasma CutterA CNC gantry plasma cutting machine moves one or more cutting stations across a guided bridge to process suitable electrically conductive plate and supported profiles. The correct configuration depends on the material, thickness, plate size, part geometry, edge quality, bevels, secondary operations, extraction, automation, and required output.
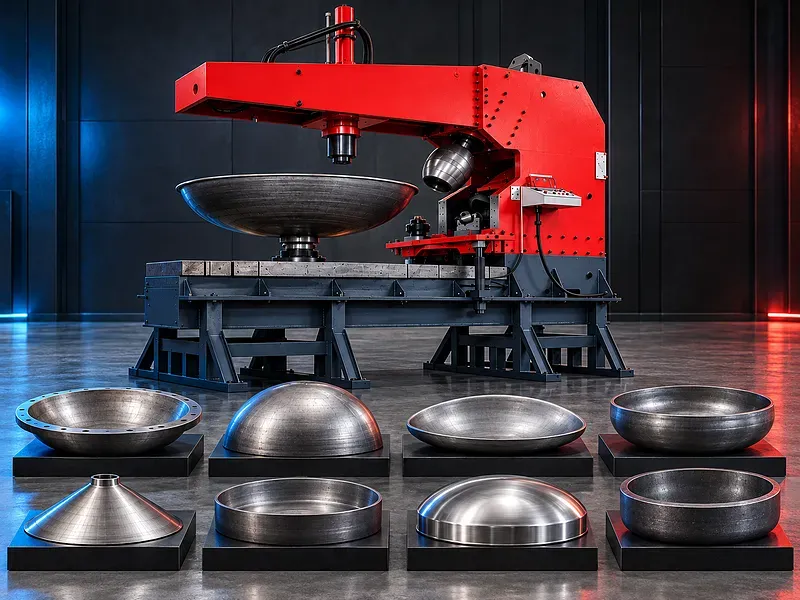 Dished Head Flanging MachineA dished head flanging machine forms the knuckle and straight flange of supported vessel heads after the blank has been prepared or dished. The correct configuration depends on the head diameter, thickness, material, profile, central opening, forming temperature, tooling, handling, tolerance, and required output.
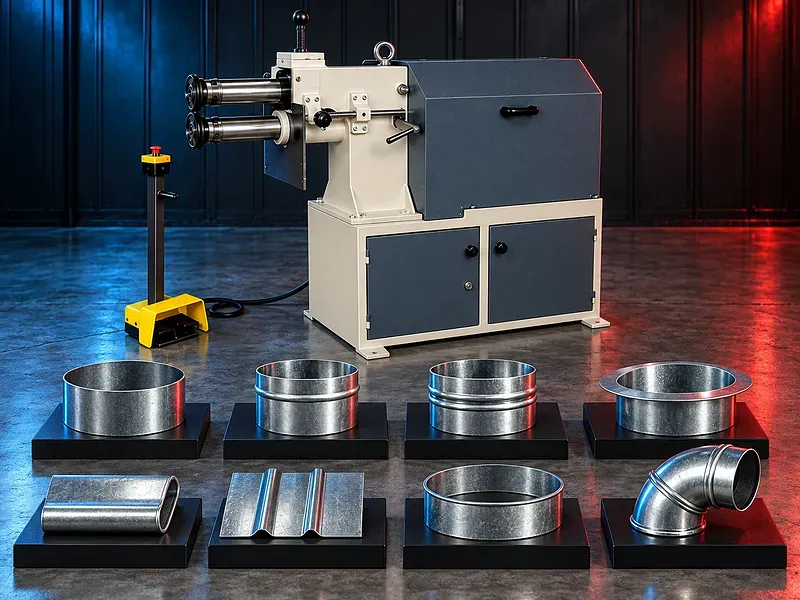 Motorized Bordering Trimming MachineA motorized bordering and trimming machine supports controlled edge finishing on compatible sheet metal parts. The correct machine and tooling depend on the part geometry, material, thickness, edge profile, dimensional tolerance, surface requirement, and production target.
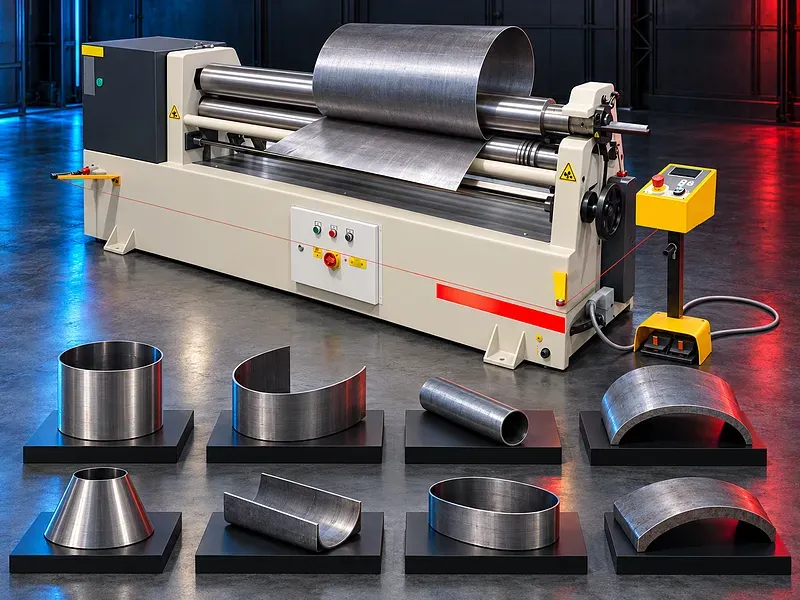 Three Roll Hydraulic Plate Bending MachineA three roll hydraulic plate bending machine forms compatible metal plate into cylinders, arcs, and supported conical shapes through controlled roll movement. Correct selection depends on material strength, plate thickness and width, target diameter, prebending requirement, geometry, tolerance, handling, and production pattern
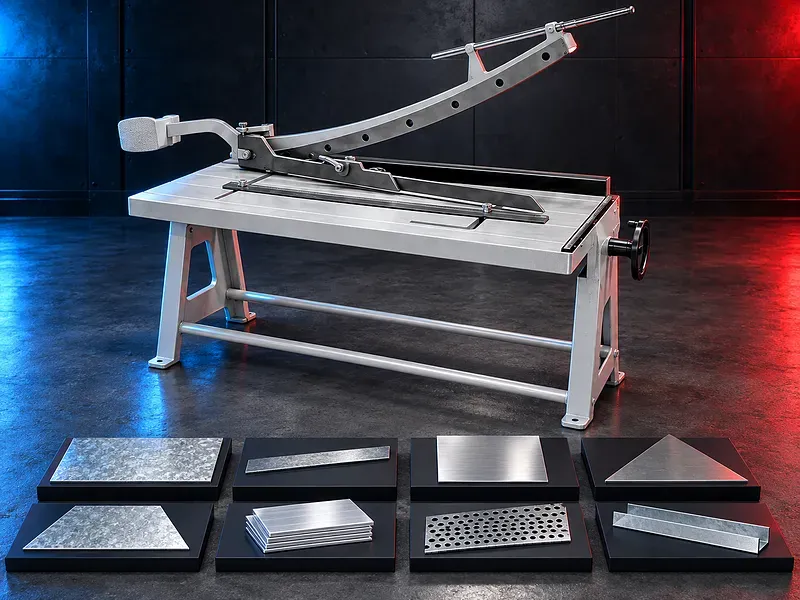 Manual Arm Guillotine ShearA manual arm guillotine shear cuts compatible sheet metal through a lever operated blade stroke. Correct selection depends on the material grade, sheet thickness, cutting length, required edge quality, clamping, gauging, operator effort, and production pattern
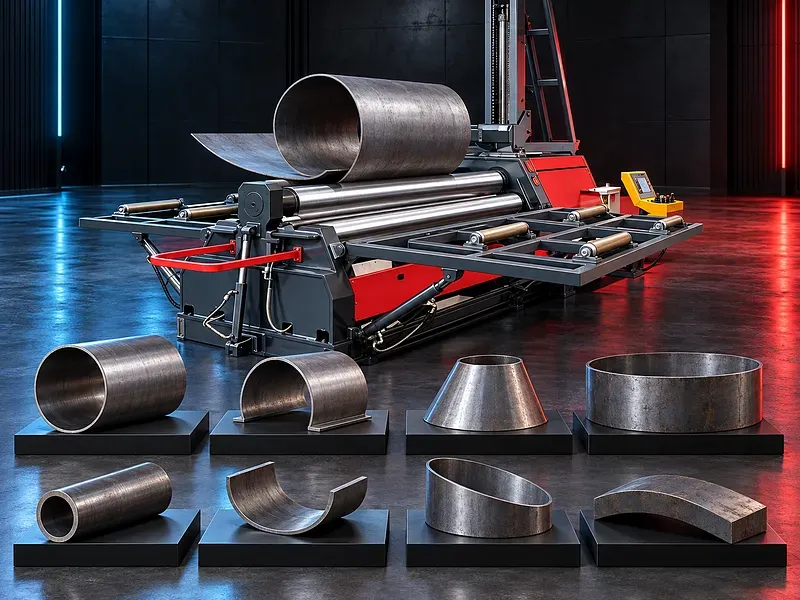 Four Roll Plate Rolling MachineA four roll plate rolling machine clamps compatible plate between upper and lower rolls while two side rolls control bending and prebending. Correct selection depends on material strength, plate thickness and width, target diameter, geometry, tolerance, supports, handling, and production requirements.
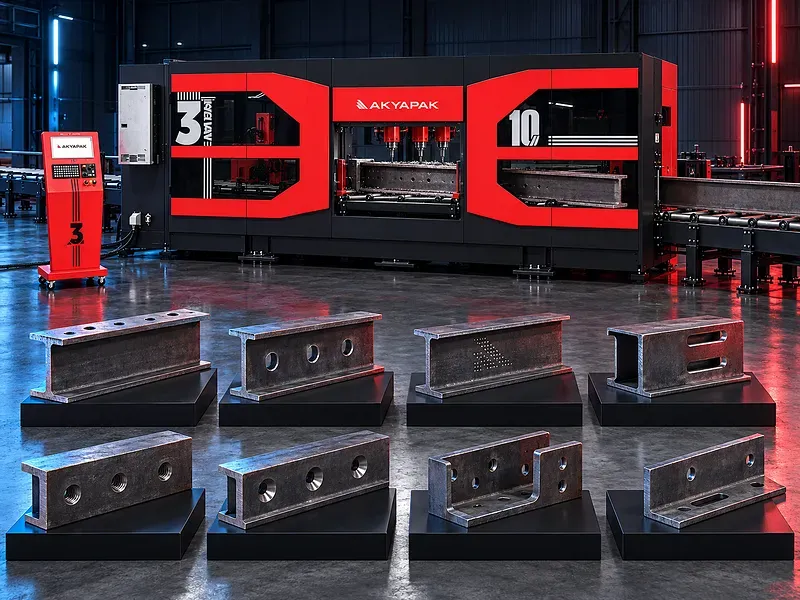 Three Spindle Beam Drill LineA three spindle CNC beam drill line processes multiple faces of compatible structural steel profiles in a controlled production flow. The correct configuration depends on profile type and size, material, hole pattern, machining operations, tolerances, tools, handling, software, output, and downstream fabrication.
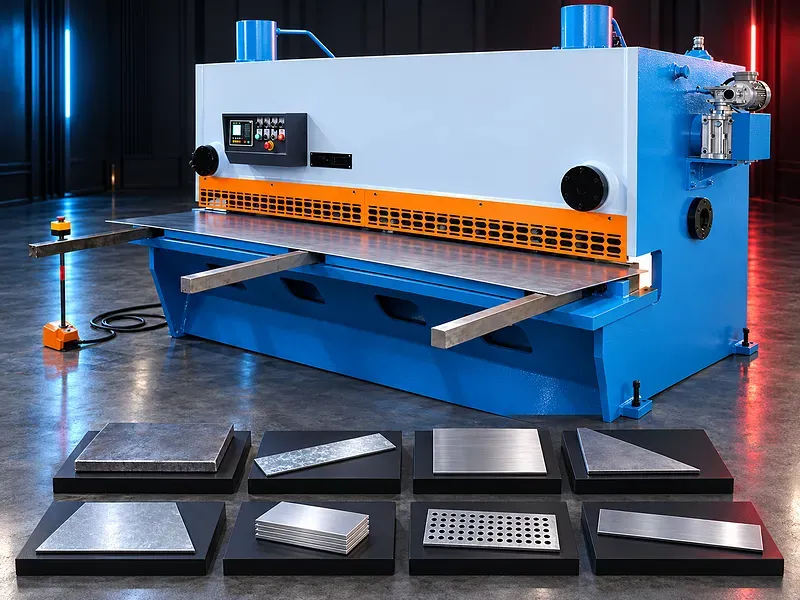 Hydraulic Swing Beam Guillotine ShearA hydraulic swing beam guillotine shear cuts compatible sheet metal through a hydraulically driven blade beam moving on a controlled arc. Correct selection depends on material strength, thickness, cutting length, edge quality, back gauge, support, anti twist requirements, output, and safety configuration.
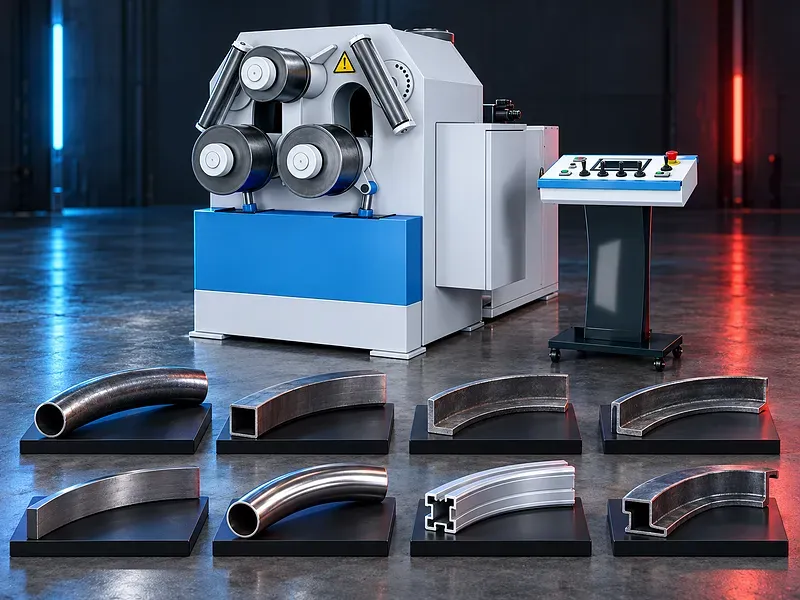 Section Profile Bending MachineSection profile bending machines form compatible metal profiles into controlled curves and rings using driven and adjustable rolls. Correct selection depends on the profile shape and orientation, material condition, section dimensions, required radius, finished geometry, batch size, handling method, and production target.
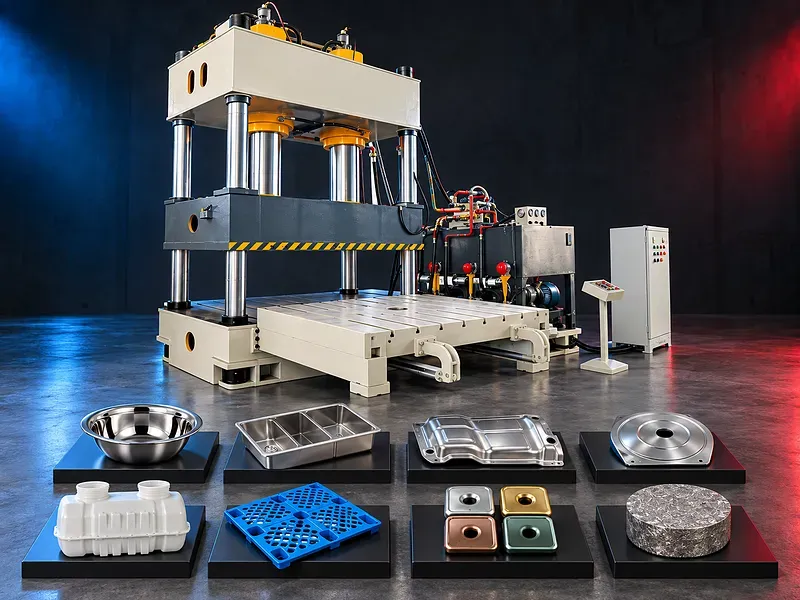 Four Column Hydraulic PressFour column hydraulic presses apply controlled pressing force through a guided moving slide for compatible forming, drawing, pressing, straightening, trimming, and assembly operations. Correct selection depends on the process, material, part geometry, required force, tooling, stroke, working space, speed, quality criteria, automation, and safety requirements
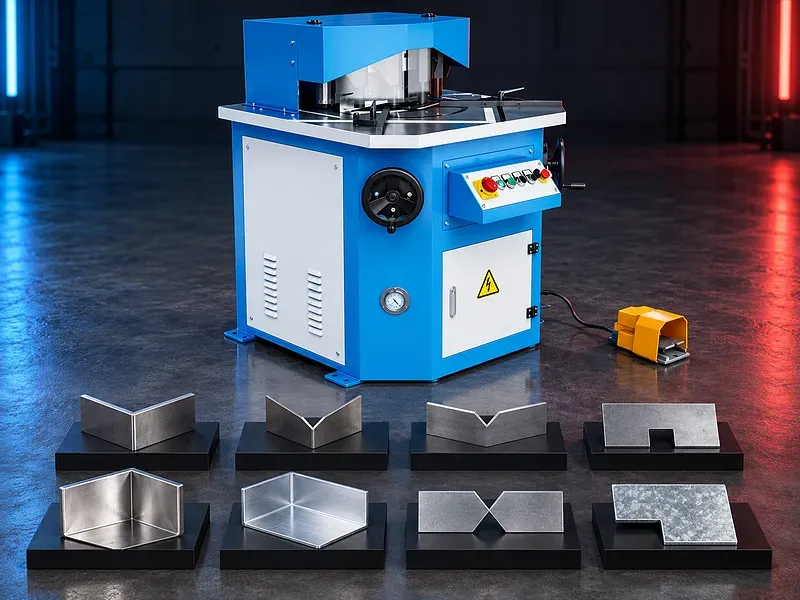 Angle Notching MachineAngle notching machines remove controlled corner sections from compatible sheet metal before bending, joining, enclosure fabrication, and other downstream operations. Correct selection depends on the material, thickness, notch dimensions, required angle, edge quality, batch size, gauges, cycle requirements, and safety provisions.
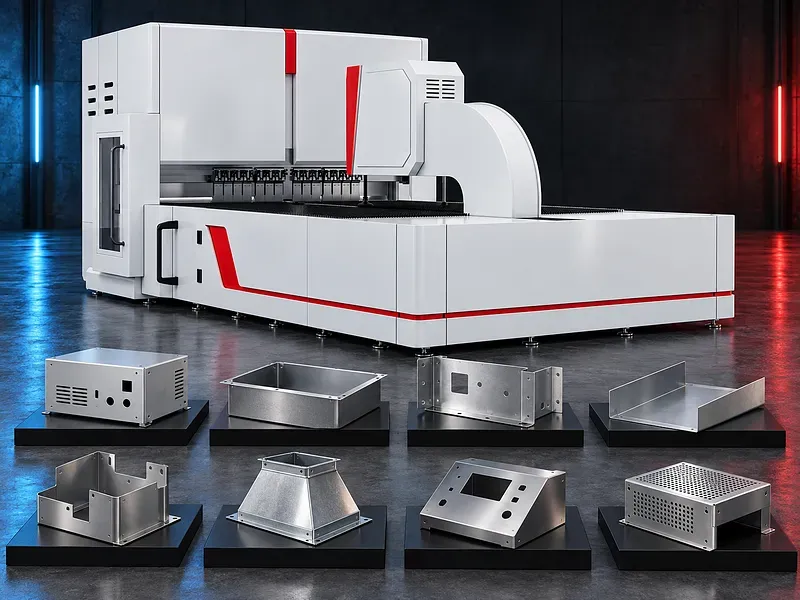 Panel Bending MachinePanel bending machines clamp, position, and form compatible sheet metal into panels, profiles, and components with multiple edges and flanges. Correct selection depends on the material, blank dimensions, bend length, flange geometry, angle, radius, sequence, tolerance, batch mix, handling method, and required output.
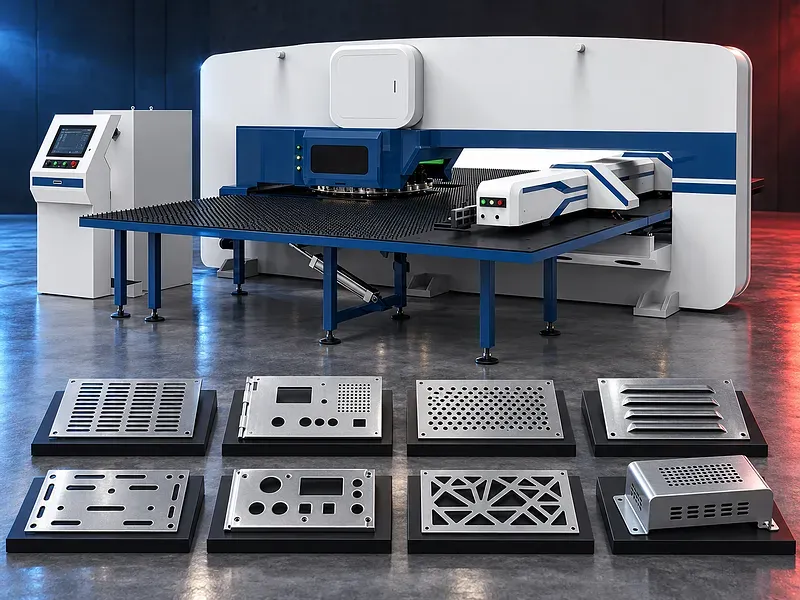 CNC Turret Punch PressCNC turret punch presses position compatible sheet metal beneath indexed punch and die tools to produce holes, cutouts, patterns, and selected formed features. Correct selection depends on the material, thickness, sheet size, part geometry, tooling, punching force, hit rate, repositioning, quality criteria, automation, and production target.
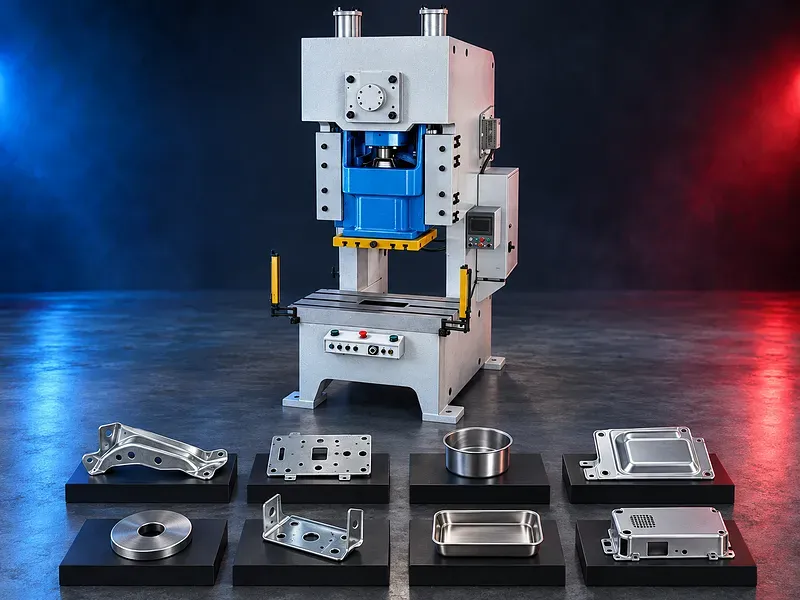 C Frame Single Crank Power PressC frame single crank power presses convert rotary motion into a repeated slide stroke for compatible blanking, punching, stamping, bending, and forming operations. Correct selection depends on the process force and energy, rated point, material, tool, stroke, speed, shut height, bed area, loading condition, feeding method, duty, and safety system
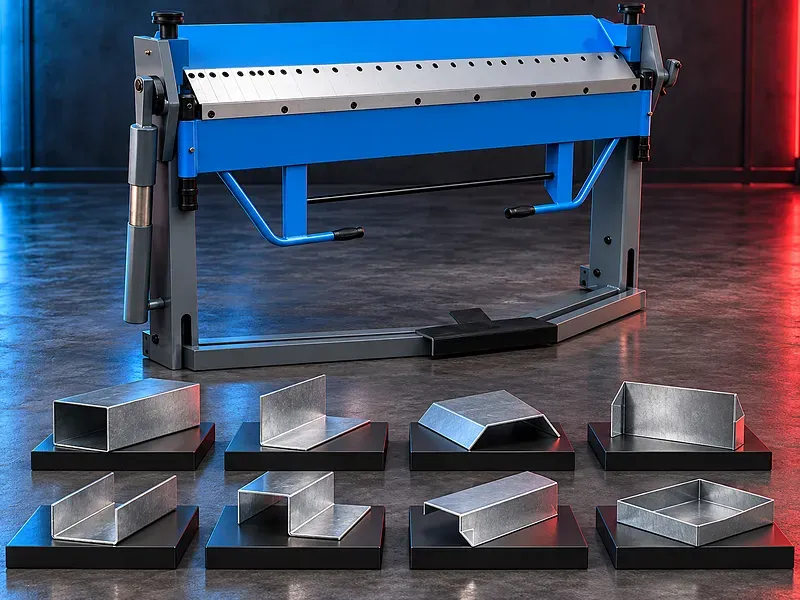 Manual Sheet Metal Folding MachineManual sheet metal folding machines clamp a compatible sheet and fold it along a straight line using an operator driven bending leaf. They are suited to selected workshop and light fabrication tasks when the material thickness working length bend geometry tooling and required accuracy remain within the approved machine limits.
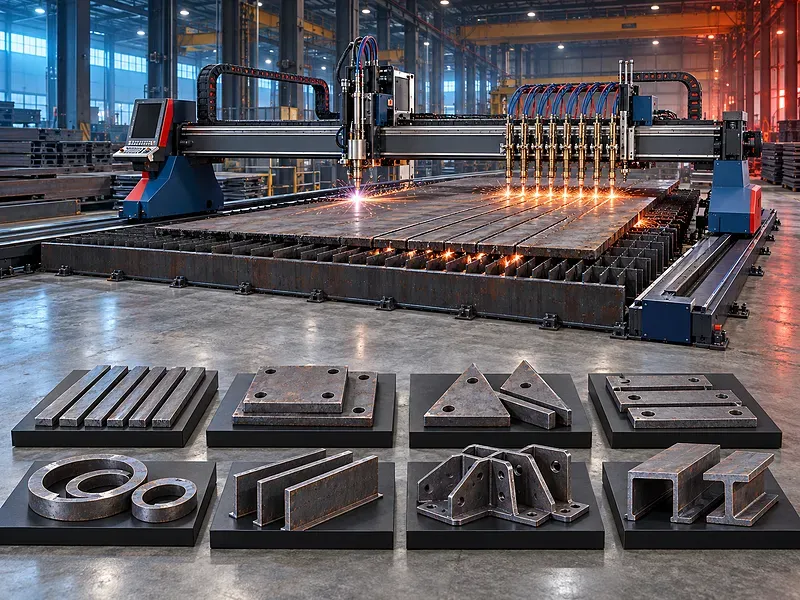 Gantry Plasma Flame Strip CutterA gantry CNC cutting machine can combine plasma profile cutting oxyfuel flame cutting and multiple parallel flame torches for compatible steel plate and strip production. Correct selection depends on material grade plate size thickness cut geometry strip widths output edge quality plasma source torch count gases extraction table layout utilities and safety requirements.
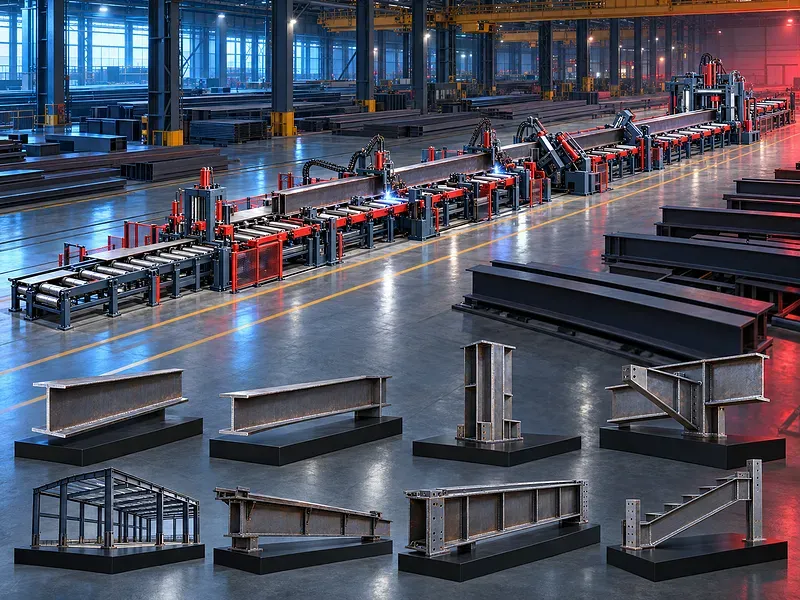 Vertical H Beam Production LineA vertical H beam automatic production line integrates plate positioning assembly welding straightening and conveying to manufacture built up steel beams through a controlled workflow. Correct selection depends on beam drawings material grades flange and web dimensions welding procedure output target quality requirements handling plan utilities and safety conditions.
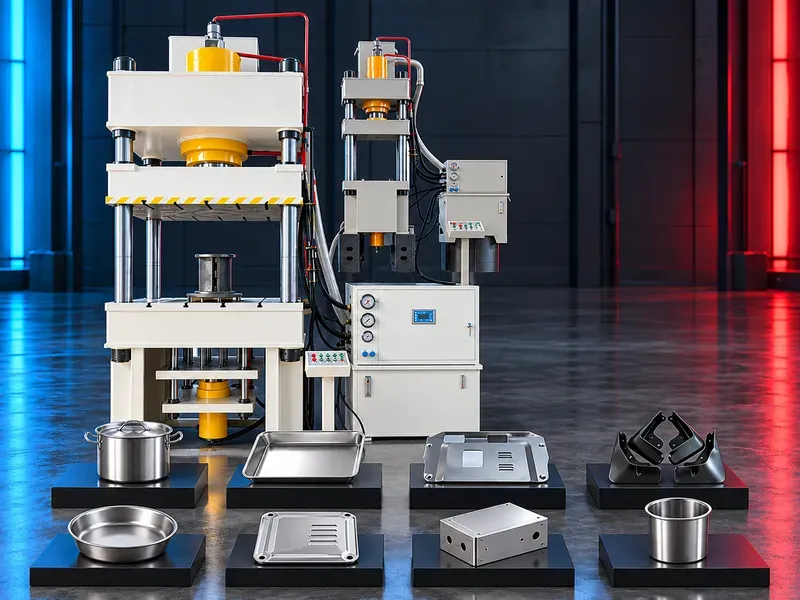 Sheet Metal Stretching Hydraulic PressA sheet metal stretching hydraulic press forms approved sheet blanks through controlled force and tool movement. Depending on the verified configuration it may support drawing blanking punching flanging and combined forming sequences for industrial components.
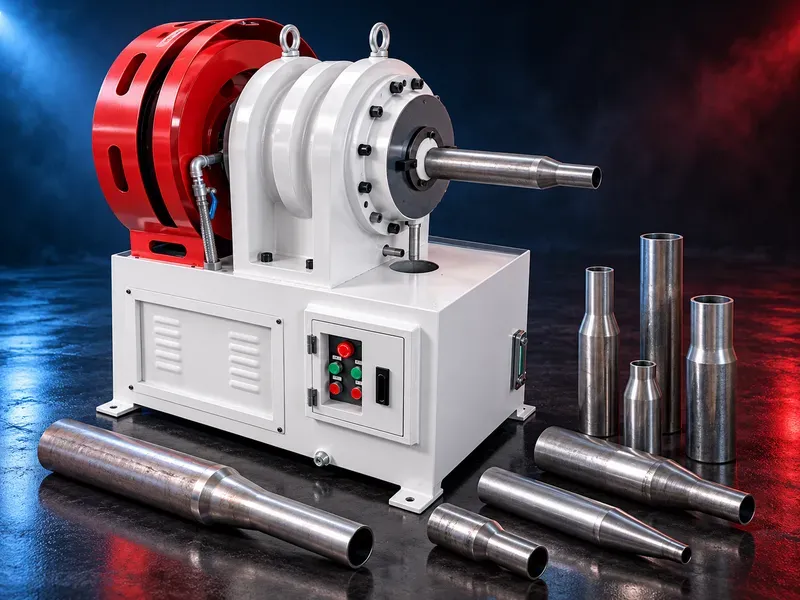 Rotary Pipe Swaging MachineA rotary swaging machine for cold-forming and tapering tube or pipe ends using a four-die rotary hammering mechanism, forming the tube progressively to the required final profile.
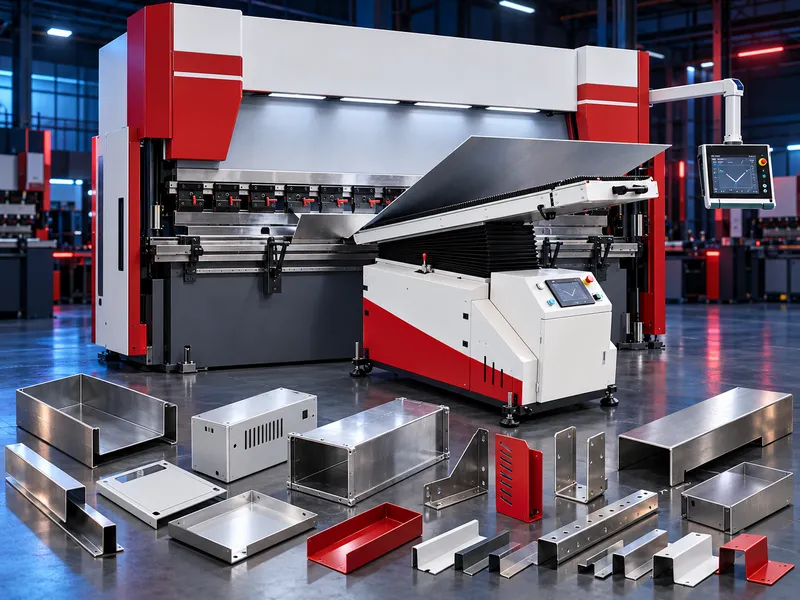 CNC Bending FollowerCNC sheet follower designed to support large sheet metal during press brake bending, following the bending movement to improve handling, reduce manual support requirements and help maintain stable workpiece positioning.
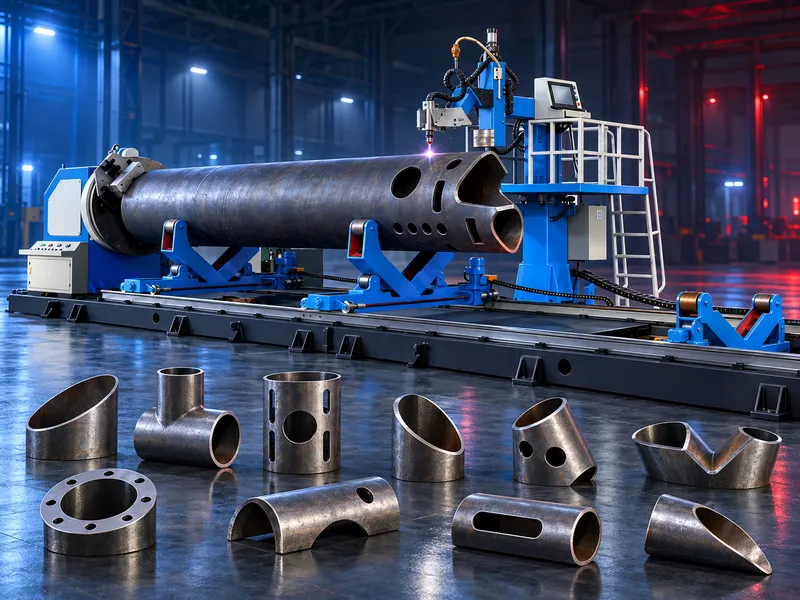 CNC Pipe Flame & Plasma Cutting MachineCNC cutting solution for metal pipes using flame and plasma cutting processes, designed for automated profile cutting and fabrication applications where controlled pipe rotation and CNC cutting are required.
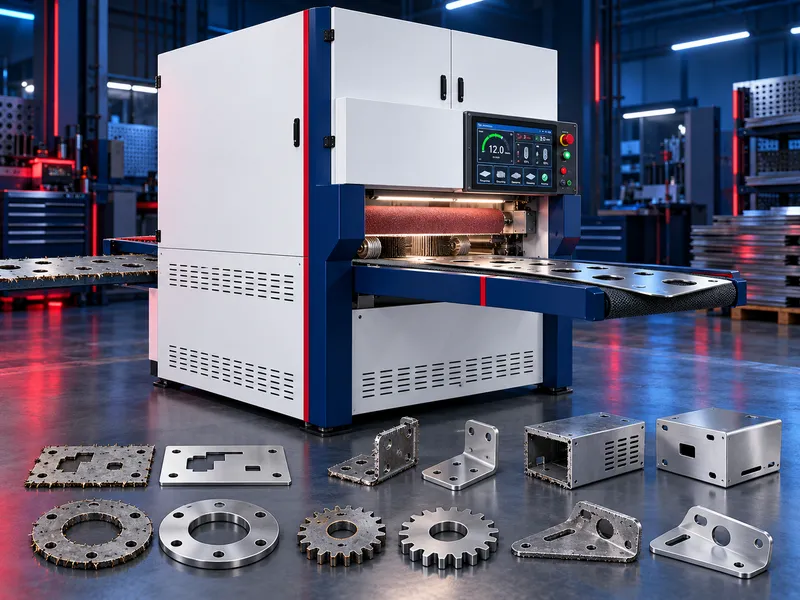 Automatic Sheet Metal Deburring MachineAutomatic finishing solution for removing burrs and sharp edges from laser-cut, punched and sheared sheet-metal parts, with configurable workholding and conveying for different materials and production requirements.
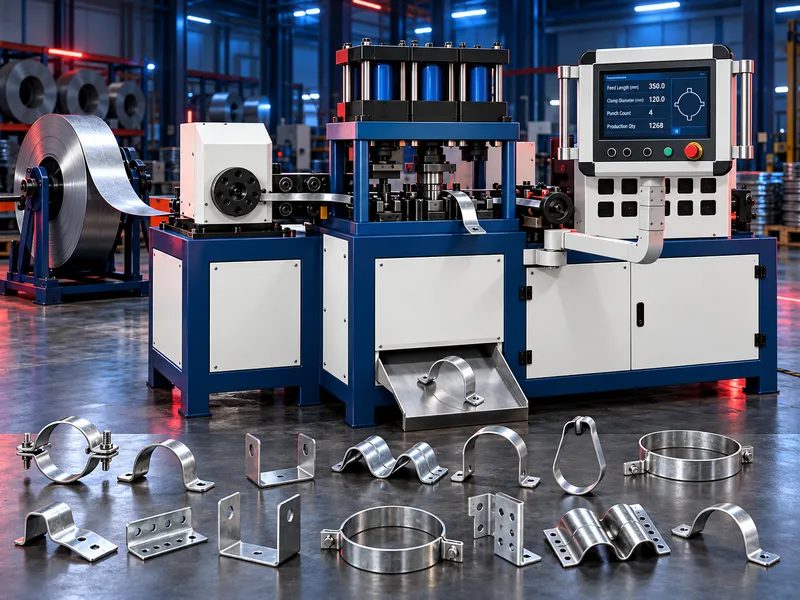 Automatic Hoop Forming MachineIntegrated forming solution combining coil feeding, strip straightening, punching, bending and cutting for automatic production of pipe clamps, support bands, mounting hoops and other formed metal-strip components
Sheet metal fabrication is a connected production route that may include blank preparation, cutting, punching, bending, rolling, forming, handling and assembly. The required machines depend on the finished product, material, thickness range, part geometry and production volume.
Selecting the correct equipment starts with the approved part drawings, material grades, sheet or plate dimensions, minimum and maximum thickness, tolerances, bend details, cut quality and required output. Tooling, automation, handling, utilities, extraction and safety must also be reviewed for the selected configuration.
What it is for
- Panels, cabinets, enclosures and ducting
- Tanks, hoppers and cylindrical vessels
- Structural brackets and gussets
- Cladding and architectural sheet work
- Repeat production of a folded part to one bend allowance
How to choose
Bending force follows material and length, not thickness alone
A long bend in stainless needs far more than the same thickness in aluminium over a short length. Tell us the worst-case bend you actually run and we size from that.
Back gauge and controller decide setup time
On short runs, the time lost setting up outweighs the time spent bending. A programmable gauge pays for itself in a job shop long before it does in a factory making one part all week.
Tooling is part of the purchase
Punches and dies are what actually make the bend. Buying a brake without budgeting the tooling for your range of radii is the most common way a good machine underperforms.
Decide where cutting happens
A shear is fast and cheap for straight cuts. A plasma or fiber table earns its place the moment parts stop being rectangles. Many shops need both, and the split is worth working out before buying either.
Questions we are asked
What information is required to select sheet metal machinery?
Provide the part drawings, material grades, sheet or plate dimensions, thickness range, required operations, tolerances, bend details, cut quality, quantities and available utilities.
How is the required press-brake capacity selected?
Selection requires the material strength, thickness, bend length, die opening, internal radius, flange geometry, tooling, cycle requirements and safety configuration.
Should I use a shear, plasma cutter or fiber laser?
A shear suits supported straight cuts. Plasma or fiber laser may suit programmed contours, depending on material, thickness, edge quality, accuracy, operating cost and downstream processes.
How is a plate rolling machine selected?
Specify the material, strength, thickness, width, required diameter, prebending, cone requirements, tolerances, supports, part weight and handling method.
Can you configure a complete sheet metal production line?
A complete line requires verified drawings, operations, output targets, factory layout, material flow, automation and utilities. The final configuration must be defined in the approved technical offer.
Are installation, training, tooling and warranty included?
The approved quotation must define installation, commissioning, training, tooling, consumables, warranty, maintenance and technical-support responsibilities.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- Fiber Laser Cutting Machines for Sheet, Tube and Profiles Fiber laser cutting solutions for suitable metal sheets, tubes and profiles, selected according to the material, dimensions, thickness, part geometry, cut requirements and production target.
- HVAC Duct Fabrication Machines Machinery for producing rectangular, round and spiral HVAC ducts, selected according to the duct drawings, material, thickness, connection system, production workflow and required output.
- Welding and Thermal Cutting Equipment Welding, robotic automation and thermal cutting solutions selected according to the material, thickness, joint or cut geometry, required quality, production volume and site conditions.