

AUTOMATIC TWO CORNER PVC PROFILE WELDING
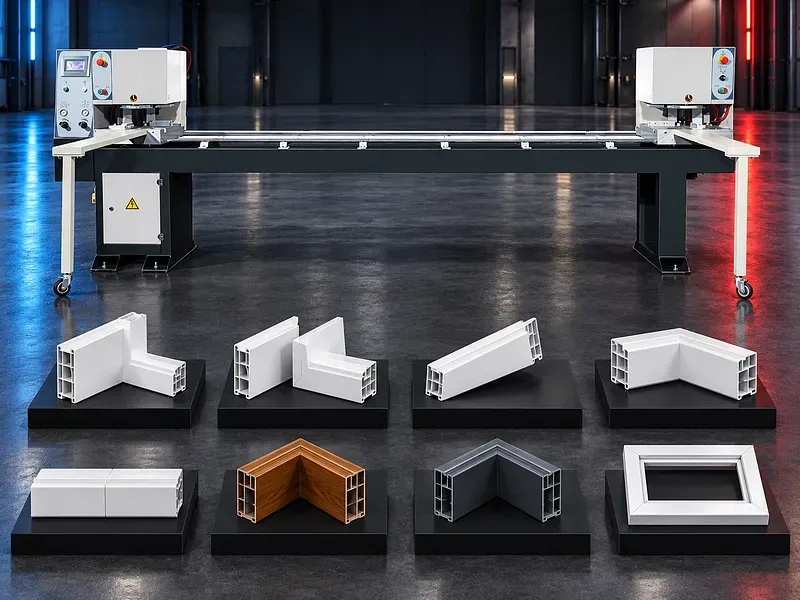
Double Corner Welding Machine for PVC Profiles
A double corner welding machine joins prepared PVC window or door profiles at two corners within a coordinated automatic cycle using fixed and movable welding heads. Correct selection depends on profile system frame dimensions head movement angle requirements joint preparation temperature pressure cycle settings support handling output utilities and safety conditions.
The operator positions prepared profiles against the head references and support arms then activates pneumatic clamping. The PLC controlled sequence heats presses holds cools and releases the two joints according to the approved program. A movable head allows the machine to adapt to approved frame dimensions while the fixed head provides a stable reference. Exact head travel angle capability cycle functions pressure ranges and included cleaning features must be confirmed from the technical documentation.
What the machine does
The machine forms two welded PVC corners in one coordinated cycle. It aligns clamps heats joins holds and cools the prepared profiles through two welding stations.
The finished result depends on profile preparation head positioning references temperature pressure time support and handling working as one process.
Fixed and movable welding heads
The fixed head establishes the primary reference while the movable head is positioned for the required approved frame dimension. Both heads must maintain alignment and consistent process conditions.
Confirm movement direction positioning method locking repeatability usable range and behavior during setup and production.
Pneumatic movement and clamping
Pneumatic devices may position clamp or actuate the welding sequence according to the supplied design. Pressure should be adjustable to secure the profile without crushing chambers or marking finished surfaces.
Air pressure quality dryness flow and filtration influence repeatability and component life.
PLC controlled automatic cycle
The PLC coordinates clamping heating plate movement joining holding cooling and release. Automatic start and completion functions can reduce manual variation when guards sensors and references are correctly set.
Verify program functions alarms manual setup mode access levels counters and safe restart after interruption.
Profile preparation
Profile ends should be cut to the approved angles and lengths with clean matching surfaces. Reinforcement seals films chips moisture and contamination must be handled according to the profile system procedure.
Incorrect preparation can cause gaps twist weak fusion excess bead or inaccurate frame dimensions.
Head angle capability
An adjustable welding angle may be provided on one head when included in the configuration. Actual angle range joint geometry and clamping arrangement must suit the approved profile system.
The stated angle capability requires confirmation from the official data sheet and sample welding trials.
Heating and thermostat control
Thermostatic control regulates the heating plate according to the process setting. Plate surface condition coating cleanliness and temperature stability influence heat transfer to both joints.
Confirm sensor arrangement temperature range calibration alarm behavior warm up time and plate replacement procedure.
Welding pressure and cycle settings
Clamp pressure welding pressure melting time joining time holding and cooling may be adjustable according to the supplied control. Settings must be validated for each approved profile family.
Both heads should deliver a consistent process so the two corners meet the same dimensional and strength requirements.
Frame support and unloading
Right and left support arms can carry the profiles and partial frame during loading welding and removal when included. Supports should prevent sagging twisting and impact on hot joints.
Define safe lifting points operator positions and the sequence for removing the welded assembly without loading the joints prematurely.
Heating plate access and replacement
A practical heating plate access arrangement can reduce maintenance time when the machine is isolated and cooled. Replacement must preserve plate alignment sensor contact and protective coating condition.
Use approved plates fasteners and setup checks before returning the machine to production.
Voltage and control protection
A voltage monitoring or protection relay may protect the control system from specified supply abnormalities when included. It does not replace correct incoming power grounding and an approved site protection design.
Confirm voltage frequency permitted variation protection sequence and restart behavior with the electrical documentation.
Corner quality and inspection
Acceptance should define both corner angles frame dimensions diagonals surface alignment gaps bead condition visible marks and joint strength according to the approved window or door system.
Inspect sample welds after setup parameter changes plate maintenance or profile changes and follow the required destructive test plan.
Production workflow
Prepared profiles should be identified loaded and supported in the correct orientation. After the two corners are welded and sufficiently cooled the partial frame moves to the next welding cleaning or assembly stage.
Practical output includes loading head positioning clamping cycle time unloading inspection profile changes and material handling.
Safety and operator protection
The machine contains hot plates pneumatic clamps moving heads and welding tables. Guards interlocks emergency stops safe control functions heat warnings and suitable protective equipment should follow the approved risk assessment.
Safe procedures must cover loading head positioning angle setup plate access hot surface cleaning jam recovery and maintenance with verified isolation.
Installation and site readiness
Site preparation should confirm a level floor electrical supply compressed air ventilation lighting profile and frame handling space and maintenance clearance. The movable head travel zone must remain protected and clear.
Arrange cutting welding cooling cleaning and storage areas to prevent contamination mixed parts and unsafe movement.
Training maintenance and lifecycle support
Training should cover head positioning profile references pneumatic settings PLC cycle parameters temperature first piece inspection safe recovery and daily care. Operators should recognize pressure loss temperature drift and joint defects.
Preventive maintenance should address heating plates coatings clamps cylinders guides head movement sensors PLC components relays seals supports guards and safety devices. Prepare an approved spare parts and consumables list.
How to select the correct machine
Start with profile system drawings section range frame dimensions angle requirements daily product mix joint quality tests support needs and downstream cleaning. Then define head travel control pressure cycle settings utilities handling and acceptance samples.
Selection should be based on two corner sample welds and approved dimensional and strength tests rather than maximum weld strength or cycle speed claims alone.
Technical information requiring verification
Verify profile section range movable head travel minimum and maximum frame dimension welding angle range clamping and welding pressure adjustment temperature range melting joining holding and cooling times weld allowance support arms cycle time compressed air electrical load dimensions and weight.
Supplier statements about head movement angle range display functions voltage protection and maximum weld strength require confirmation from an approved data sheet. Confirm installation commissioning training warranty service scope spare parts and acceptance tests.
Publishing status
This page describes the machine category and selection logic. Exact travels angles temperatures pressures times strength accuracy productivity functions options standards and commercial commitments require an approved data sheet and technical review before publication.
Questions we are asked
What is a double corner welding machine?
It is a PVC profile welding machine that produces two frame corners in one coordinated cycle using fixed and movable welding heads.
How does the automatic cycle work?
The profiles are referenced clamped heated pressed held cooled and released through a PLC controlled sequence.
Why does one head move?
The movable head adjusts the distance between welding stations to suit approved frame dimensions while the fixed head provides a reference.
Can welding angles be adjusted?
An adjustable angle may be available on one head but the actual range and compatible joints require confirmation from the technical data.
How is weld quality verified?
Check both corner angles frame dimensions diagonals surface alignment bead condition appearance and joint strength against the approved profile system.
What information is needed for selection?
Provide profile system drawings section range frame sizes angle needs product mix quality tests support requirements utilities and site layout.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- Aluminum Profile End Milling Machine End milling solutions for preparing aluminum profile ends for accurate fitting and assembly in suitable window, door and facade systems.
- Automatic Up Cut Mitre Saw for Aluminium and PVC An automatic up cut mitre saw uses a guarded blade that rises through the work area to cut approved aluminium and PVC profiles at straight or angled settings supported by the machine. Correct selection depends on profile material cross section length cut angles finished quality blade clamping feeding cooling extraction output target utilities and safety requirements.
- Double Head Mitre Saw for Aluminium and PVC A double head mitre saw cuts both ends of an approved aluminium or PVC profile to the required length and supported angles within one coordinated cycle. Correct selection depends on profile material cross section finished length angle combination cut quality blade configuration head positioning clamping support output utilities and safety requirements.