

ACCURATE PROFILE CUTTING FOR ALUMINIUM AND PVC
Automatic Up Cut Mitre Saw for Aluminium and PVC
An automatic up cut mitre saw uses a guarded blade that rises through the work area to cut approved aluminium and PVC profiles at straight or angled settings supported by the machine. Correct selection depends on profile material cross section length cut angles finished quality blade clamping feeding cooling extraction output target utilities and safety requirements.
The workpiece is positioned against the machine references and secured before the blade enters the profile from below. The guarded upward cutting movement can support a controlled cut while keeping the blade enclosed when it is outside the cutting cycle. The machine may be used for window door facade partition and furniture profile preparation when the material and section are approved. Exact angle positions cutting envelope automation and accessories must be confirmed from the technical documentation.
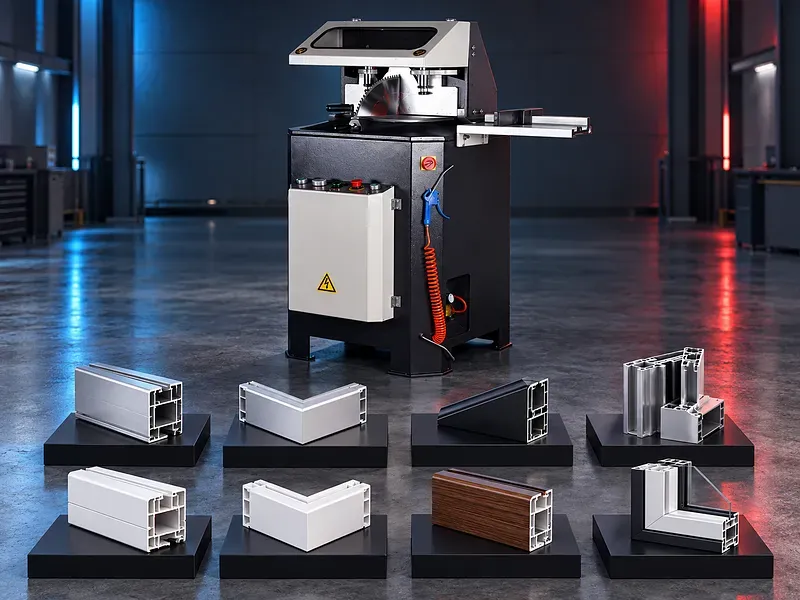
What the machine does
The saw positions and clamps a prepared profile then raises the rotating blade through the programmed or selected cutting path. After the cut the blade returns to its guarded position before the clamps release according to the approved control sequence.
The result depends on profile support blade selection angle setting clamping feed motion lubrication chip control and inspection working together.
Up cut working principle
In an up cut arrangement the blade approaches the profile from below the support surface. The machine structure and guard isolate the blade before and after the cutting movement.
Blade rise speed cutting feed and return sequence must suit the material wall thickness profile shape and selected blade.
Straight and mitre cutting
The saw may perform square cuts and approved mitre angles when the head or reference system is set for those positions. Available angles and whether positioning is manual pneumatic or controlled vary by configuration.
Confirm angle range indexing method locking repeatability and calibration using the actual profiles and joint drawings.
Aluminium profile applications
Approved aluminium extrusions for windows doors facades partitions furniture and industrial assemblies may be cut when their alloy temper geometry and wall thickness suit the blade and machine envelope.
Thin walls chambers thermal breaks surface finishes and protective films require suitable support clamping blade geometry and lubrication.
PVC profile applications
Approved rigid PVC profiles may be cut for window door and related fabrication when the blade tooth form speed support and clamping prevent melting cracking or deformation.
Profiles with reinforcement seals films or inserted components require a specific process review because the combined materials can change cutting behavior.
Profile support and positioning
The profile should rest against stable fences and supports so the cut reference remains square and the section does not twist. Long stock may require roller tables length stops measuring systems or automatic feeding.
Confirm infeed and outfeed length support height reference side and handling of short offcuts and long flexible profiles.
Automatic clamping
Clamps secure the profile before blade movement and should release only after the blade returns to the safe position. Clamp layout and pressure must prevent movement without crushing hollow or finished sections.
Verify horizontal and vertical clamping pressure adjustment contact pads sensors and compatibility with the full product family.
Blade selection
Blade diameter bore tooth count tooth geometry kerf material and maximum approved speed must match the saw and profile. Aluminium and PVC may require different blade designs even when processed on the same machine.
Use only approved sharp balanced blades and follow a documented sharpening replacement and inspection plan.
Lubrication cooling and chip control
Aluminium cutting may require an approved minimum quantity lubricant or another specified method to control heat chip adhesion and surface finish. PVC cutting needs a process that avoids excessive heat and material smearing.
Confirm lubricant compatibility application points collection method chip extraction and cleaning routine for the selected materials.
Cut quality and inspection
Acceptance should define cut length angle squareness burr level edge finish deformation and joint fit from the finished product drawing. The first piece should be measured before batch production continues.
Blade condition profile variation support and temperature can influence the result even when the machine setting is unchanged.
Cycle and productivity
Practical output includes loading positioning clamping cutting return unloading measurement and material handling. Automation can reduce cycle variation but does not remove the need for correct preparation and inspection.
Evaluate productivity with representative profiles cut lists angle changes batch sizes offcut rules and operator tasks.
Safety and operator protection
The machine contains a high speed saw blade automatic clamps sharp profiles and ejected chips. Guards interlocks emergency stops safe control functions and eye hearing and hand protection should follow the approved risk assessment.
Safe procedures must cover loading angle setup blade changes trial cuts offcut removal cleaning jam recovery and maintenance with verified isolation.
Installation and site readiness
Site preparation should confirm a level floor electrical supply compressed air when required lubrication or cooling arrangements chip extraction lighting and sufficient space for the longest profile and handling equipment.
Install infeed and outfeed supports at the correct height and provide safe routes for raw profiles finished parts and scrap.
Training maintenance and lifecycle support
Training should cover profile references angle settings clamps blade inspection lubrication quality checks safe recovery and daily care. Operators should recognize blade noise vibration heat and finish changes before damage develops.
Preventive maintenance should address blades spindle bearings belts or drives guides clamps cylinders sensors lubrication extraction guards and safety devices. Prepare an approved spare parts and consumables list.
How to select the correct machine
Start with profile drawings materials maximum cross sections stock lengths required angles cut list volumes batch sizes tolerances surface protection and downstream joining. Then define supports feeding measuring lubrication extraction utilities and acceptance samples.
Selection should be based on representative profiles and verified cuts rather than blade diameter or an unsupported cycle time alone.
Technical information requiring verification
Verify the cutting envelope for every required angle profile length and minimum offcut. Also verify blade diameter bore speed motor power angle positions feed system clamping pressure cut accuracy cycle time lubrication extraction compressed air electrical load dimensions and weight.
Confirm included blades supports stops measuring devices guarding installation commissioning training warranty service scope spare parts and the agreed acceptance tests.
Publishing status
This page describes the machine category and selection logic. Exact capacities angles speeds accuracy productivity features options standards and commercial commitments require an approved data sheet and technical review before publication.
Questions we are asked
What is an automatic up cut mitre saw?
It is a profile cutting machine that clamps the workpiece and raises a guarded blade from below to make an approved straight or angled cut.
Can one machine cut aluminium and PVC?
It may process both when the exact configuration blade speed lubrication support and clamping are approved for each material. Separate blades or setups may be required.
Which angles can it cut?
The available straight and mitre positions depend on the supplied head and positioning system. The required angles must be confirmed from the technical data.
How is the profile held during cutting?
Automatic clamps hold the profile against the references before blade movement and release it only after the safe return sequence.
What affects cut quality?
Blade design and condition profile support clamping feed speed lubrication material geometry and temperature all influence angle edge finish burrs and deformation.
What information is needed for selection?
Provide profile drawings materials cross sections stock lengths angles cut lists quantities tolerances surface requirements handling utilities and site space.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- Aluminum Profile End Milling Machine End milling solutions for preparing aluminum profile ends for accurate fitting and assembly in suitable window, door and facade systems.
- Double Head Mitre Saw for Aluminium and PVC A double head mitre saw cuts both ends of an approved aluminium or PVC profile to the required length and supported angles within one coordinated cycle. Correct selection depends on profile material cross section finished length angle combination cut quality blade configuration head positioning clamping support output utilities and safety requirements.
- Portable Copy Router and End Milling Machine for Aluminium and PVC Portable copy routing and end milling equipment is used to machine approved openings slots recesses and profile ends for aluminium and PVC fabrication. Correct selection depends on whether the required functions are combined or supplied separately as well as profile material geometry machining detail template or stop system tooling clamping quality output utilities and safety requirements.