

DECORATIVE PROFILE FINISHING
Profile Wrapping Machines for PVC Film
Profile wrapping machines apply compatible decorative film or paper to straight continuous profiles by controlling adhesive coating film guidance and pressure roller forming around the cross section. Correct selection depends on the profile material geometry dimensions surface film adhesive speed finish requirement production mix utilities and installed processing units
The process feeds a prepared profile through an adhesive and film application sequence then uses adjustable rollers positioned around the cross section to press the decorative material onto compatible faces edges curves and returns. Roller layout must be developed for the actual profile and film. Potential applications include selected profiles used in furniture doors windows interior finishing tabletops and building products. PVC film decorative paper and other covering materials require exact compatibility approval through supplier instructions and a production trial.
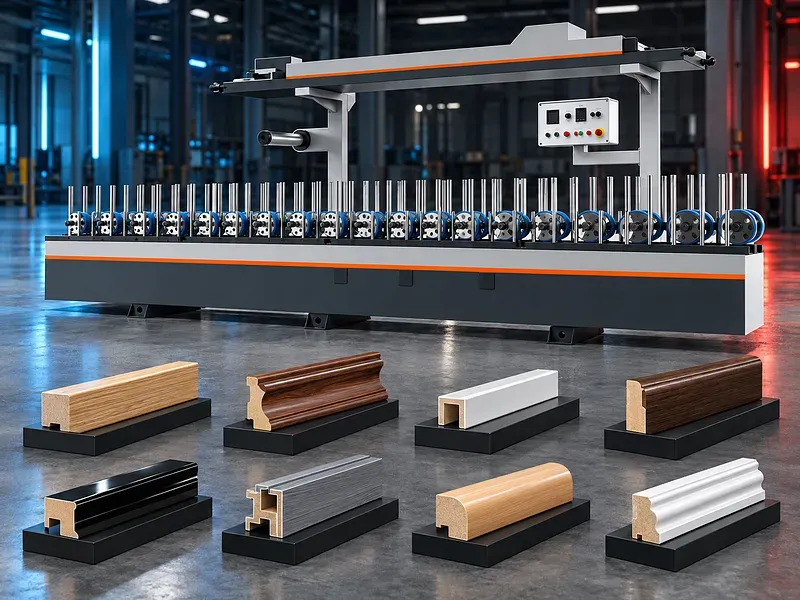
What a profile wrapping machine does
The machine bonds a flexible decorative covering to the surface of a compatible straight profile while the workpiece moves continuously through guided roller stations. Each roller presses a defined area of the film onto the cross section.The installed coating heating guiding and forming units determine the supported materials and process. The machine does not create the substrate shape and does not guarantee that every complex profile can be wrapped.Potential profile materials
Potential substrates may include compatible wood based profiles medium density fiberboard solid wood plastics selected metal profiles and composite products when the surface and process are approved.Material name alone is not enough for approval. Surface energy porosity moisture coating contamination temperature sensitivity stiffness dimensional stability and adhesive compatibility should be reviewed.Profile geometry and dimensions
Wrapping suitability depends on profile width height length face layout edge radius grooves returns undercuts and the sequence in which the film reaches each surface. Sharp corners deep recesses and reverse curves may limit film contact or require special rollers.Provide a dimensioned cross section drawing and physical samples. The roller plan film width adhesive method and trial criteria should be developed from the exact geometry.Decorative films and papers
Potential covering materials may include selected PVC film decorative paper veneer foil and other flexible products when approved for the machine adhesive profile and finished use.
Confirm film thickness width roll diameter core size print direction stretch behavior protective layer primer back treatment heat limit storage condition shelf life color match and supplier instructions.Profile surface preparation
The profile should be straight clean dry dimensionally stable and free from dust oil chips loose fibers release agents and surface defects. Sanding cleaning priming or sealing may be required according to the substrate and adhesive.Surface preparation should be validated because the same adhesive can perform differently on porous coated plastic or metal surfaces.Adhesive selection
The adhesive should be selected for the substrate film production speed working temperature finished product duty and environmental exposure. Potential systems may include approved cold adhesives or hot melt technologies depending on the machine configuration.Mixing viscosity solids content coating weight open time activation temperature curing cleaning storage ventilation and safe handling must follow the adhesive supplier data.Adhesive coating system
A coating unit may apply adhesive to the film or substrate through rollers a doctor blade scraping arrangement nozzles or another verified method. Uniform coating supports consistent wetting without excessive squeeze out.The exact coating design pump reservoir roller gap blade setting width adjustment filtration recirculation cleaning and changeover method require confirmation.Film unwind tension and alignment
The unwind station feeds the covering material under controlled tension so it enters the wrapping zone without wrinkles tracking drift or uncontrolled stretch. Roll mounting braking guides and sensors influence alignment.An edge guiding or correction device may adjust film position during operation when included. Correction range response accuracy and behavior at joints or roll changes must be verified.Heating and activation
Auxiliary heaters may warm the profile film adhesive or forming zone when required by the approved process. Heating can support activation flexibility or climate compensation but excessive heat may distort film damage print or change adhesive behavior.Confirm heater type location power temperature range sensors airflow shielding warm up time ambient conditions and fire controls.Forming and pressure rollers
Adjustable rollers contact the film progressively around the profile. Roller material hardness diameter shape angle position and pressure should match the cross section without marking the visible surface or trapping air.Standard rollers may not fit every profile. Special shaped rollers templates setup records and sample approval may be required for stable changeover and repeat production.Drive and speed control
The drive moves the profile and may coordinate adhesive film and roller stations at an adjustable line speed. Stable transport depends on drive layout roller traction profile support alignment and verified speed control.Confirm speed range drive motors transmission arrangement variable speed method synchronization load limits and behavior during start stop and faults.Exit support curing and trimming
The wrapped profile may need supported travel while the bond develops. Depending on the product it may also require edge trimming end cutting cooling conditioning or protected storage before downstream processing.Define minimum curing or conditioning time stacking method temperature handling limits inspection point and permitted next operation from the adhesive instructions and trials.Electronic control and automation
The control system may manage line speed heaters adhesive units film correction sensors alarms and stored settings according to the installed configuration. Loading profile feeding roll changes cleaning and some setup may remain manual.Confirm interface language recipes automatic positioning sensor logic fault handling data recording permissions diagnostics network options and backup procedures.Production workflow
Begin with approved profile film and adhesive specifications a dimensioned cross section roller setup sheet coating settings and inspection plan. Check profile condition adhesive preparation film direction guides rollers heaters extraction and safety functions.Run a sample profile inspect alignment adhesion corners grooves seams wrinkles bubbles glue residue surface marks and dimensions apply approved corrections then release production with regular checks.Quality and acceptance
Inspection may cover film position joint alignment adhesion peel behavior corner contact groove contact bubbles wrinkles stretching print distortion glue marks surface damage gloss color match edge lift and finished dimensions.The control plan should define conditioning test method acceptance limits sampling destructive tests where required first piece approval traceability and handling of nonconforming profiles.Potential applications
Potential applications include compatible furniture trims cabinet profiles door and window components decorative mouldings tabletop edges wall and ceiling profiles and selected building finish products.Suitability depends on profile geometry substrate film adhesive visual standard environmental duty downstream cutting drilling assembly packing and installation conditions.How to choose the correct machine
Provide profile material and cross section drawing minimum and maximum dimensions length surface condition film type thickness width and roll data adhesive process production quantities batch mix finish standard and target output.Also define coating method heating needs special roller sets edge correction trimming curing extraction compressed air electrical supply floor space staffing maintenance capability and acceptance tests.Technical information to verify
Approved documents must confirm profile width height and length ranges supported geometries film width roll diameter core size film thickness adhesive systems coating method line speed roller station quantity roller adjustment heating units correction device and control functions.Motor power electrical load compressed air ventilation extraction dimensions weight floor loading noise basis guards safety functions standard equipment options special rollers tools consumables documents training warranty service and acceptance method also require confirmation.Safety and environmental controls
Risks include rotating rollers pinch points moving profiles film unwind moving chains or gears hot surfaces heaters adhesive chemicals fumes solvents compressed air electrical energy sharp edges jams and cleaning or maintenance work.The installation needs approved guards interlocks emergency stops safe threading and setup procedures isolation ventilation extraction fire controls adhesive handling personal protection spill response training supervision and a documented risk assessment.Installation and commissioning
Site preparation should cover delivery access level floor line clearance electrical supply compressed air ventilation extraction climate control adhesive and film storage profile infeed and outfeed areas waste collection fire controls and maintenance access.Commissioning should verify alignment transport speed coating distribution film tracking heater control roller setup sensors controls safety functions sample profiles adhesion and finish tests operator training maintenance training documents and an agreed acceptance trial.Maintenance and lifecycle support
Preventive maintenance should follow approved schedules for unwind brakes guides tension devices rollers bearings chains gears drives coating units pumps reservoirs heaters sensors correction devices extraction guards and safety controls.Agree recommended roller materials coating parts blades seals pumps heaters sensors belts chains bearings filters cleaning agents approved lubricants software backups setup records technical documents training and service responsibility.Limitations and publishing status
The supplied description does not verify profile and film compatibility coating system origin accuracy transmission stability component material wear resistance temperature resistance film correction performance scrap reduction automation level labor reduction output adhesion or surface quality.Publication requires the exact approved datasheet configuration profile and film samples adhesive data roller plan sample test results safety and ventilation requirements approved image technical review staging review and final content approval.Technical review and next step
Send dimensioned profile drawings physical samples film and adhesive data production mix finish criteria target output utilities and factory layout for technical review.The review should define the suitable configuration coating method roller plan heating correction controls handling curing inspection acceptance trial installation training maintenance consumables and spare parts scope.Questions we are asked
What is a profile wrapping machine?
It is a finishing machine that bonds a compatible flexible decorative material to a straight profile through adhesive application guidance and progressive pressure rollers.
Can it wrap complex profile shapes?
Some multi face curved and grooved profiles may be suitable after the exact cross section film adhesive and roller plan pass a production trial. Deep recesses sharp corners and undercuts may limit the process.
Which covering materials can be used?
Potential materials include selected PVC film decorative paper veneer and foil only when their dimensions backing treatment adhesive temperature and flexibility match the approved process.
Does the machine operate without an operator?
Not necessarily. Controls may automate speed heating coating and film correction while loading roll changes setup cleaning inspection and fault recovery may remain manual.
What information is needed for selection?
Provide the profile cross section and sample substrate film and adhesive data dimensions production mix finish standard target output utilities and factory layout.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- CNC WOOD ROUTER CNC routing solutions for cutting, drilling, engraving and machining suitable wood panels and furniture components.
- CNC ROUTER WITH ROTARY A CNC router equipped with a rotary attachment or axis for machining suitable cylindrical and shaped workpieces. Selection depends on the part geometry, material, dimensions, required operations, accuracy, and production volume.
- Automatic Edge Banding Machines Automatic edge banding machines apply and finish compatible edge material on straight panel edges through a controlled production sequence. Correct selection depends on the panel material dimensions edge tape adhesive production volume finish requirement installed processing units utilities and extraction system.