

INTEGRATED CABINET MANUFACTURING
Integrated Cabinet Manufacturing Production Line
A cabinet production line connects cabinet design panel optimization cutting identification edge banding boring hardware preparation and assembly into a controlled order based workflow. The correct line depends on cabinet families component construction panel and edge data hardware quality output batch size software automation handling utilities staffing and factory layout.
A cabinet line may combine software controlled cutting or nesting part labeling edge banding boring drilling hardware preparation and handling according to the approved process. The aim is to keep cabinet sides tops bottoms shelves doors and backs linked to their order while reducing unnecessary movement rework and material waste. The exact machine sequence is not universal. Base cabinets wall cabinets wardrobes office storage and custom units require different routings hardware data finishes and quality checks. The line should be designed from cabinet families bills of materials and a measured production target.
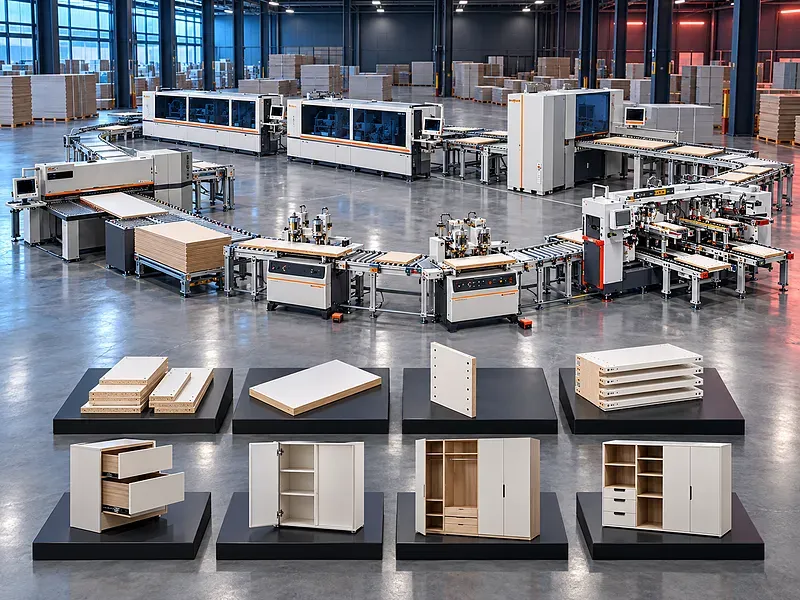
What a cabinet production line does
The line converts approved cabinet designs and panel stock into identified sides tops bottoms shelves doors and backs ready for edge treatment boring hardware preparation assembly and packing. Integration should preserve part identity dimensions orientation finish and order sequence.
The line is a production system rather than a fixed group of machines. Its value depends on balanced operations accurate data disciplined material flow and verified acceptance criteria.
Cabinet families and component structure
Define base units wall units tall cabinets wardrobes office storage vanities shelving doors and custom units. Record carcass construction component families dimensions backs shelves fronts batch sizes customization finishes and hardware.
Mixed cabinet families can create different bottlenecks. A standard carcass side may follow a different route from a shaped front glass door or pressed decorative component.
Panel materials and incoming quality
Confirm MDF type thickness density surface coating panel dimensions flatness moisture edge condition storage method and permitted defects. Also identify other boards laminates back panels and protective films used in the same workflow.
Incoming inspection should prevent warped damaged incorrectly labeled or contaminated panels from entering an automated process.
Design optimization and production data
Software may convert designs into bills of materials cutting patterns labels machining files and reports. Optimization can support better panel utilization but results depend on correct stock data grain direction kerf trim allowances priorities and reuse rules.
Confirm software functions licenses languages file formats machine interfaces revision control backups user permissions and error recovery. Integration claims require a tested data flow.
Cutting nesting and part identification
Cutting may use a panel saw sliding table saw or CNC nesting process according to part geometry volume and flexibility. Verify panel size thickness stack height tooling cut quality accuracy cycle and offcut policy for the selected equipment.
Every part should receive a durable identifier linked to the order dimensions edge instructions drilling program and assembly position. Label accuracy and scan recovery are essential.
Edge banding
Edge banding applies approved edge material and may include pre milling gluing pressing end trimming top and bottom trimming scraping and buffing. Results depend on board edge quality adhesive edge type temperature feed settings and maintenance.
Define visible edges edge thickness colors adhesive system finish acceptance and changeover rules. Do not assume one configuration processes every edge material.
Boring drilling and hardware preparation
Boring equipment creates construction holes hinge positions dowel patterns connectors grooves or other approved features from verified machining data. Datum strategy orientation tool condition and panel support affect accuracy.
Confirm drilling faces tool layout hole ranges program transfer inspection gauges and compatibility with the selected hardware system.
Cabinet assembly and special processes
Assembly may include dowels connectors screws hinges runners backs shelves doors and final hardware according to the approved cabinet system. Jigs presses or manual stations should protect squareness surfaces and part identity.
Routers presses hinge drills or other stations may be added only when required. The uploaded graphic illustrates possible cabinet machinery but does not prove the final line composition.
Material flow layout and work in process
Plan receiving storage panel feeding cutting buffers edge banding boring inspection assembly packing rework scrap and finished goods as one flow. A compact layout is useful only when access safety maintenance and buffer needs remain adequate.
Confirm aisle widths lifting routes operator positions carts conveyors scanners rack capacity and traceability between stations.
Dust extraction utilities and safety
Define extraction airflow and connections for each machine plus electrical supply compressed air vacuum cooling adhesive handling lighting network and environmental limits. Utilities must support simultaneous operation.
Risk controls should cover rotating tools moving panels clamps conveyors hot surfaces adhesives dust noise electrical energy lifting fire emergency stops guarding interlocks isolation and safe maintenance.
Quality control and traceability
Inspection should cover material identity dimensions squareness cut finish edge adhesion trimming hole position orientation surface damage completeness and order quantity. Define gauges sampling first piece approval correction limits and nonconforming control.
Traceability should connect the design revision panel batch programs labels machine results rework and final assembly.
Output cycle balance and staffing
Line output depends on product mix panel yield cutting patterns edge count drilling density changeovers rejects maintenance material supply buffers operator skill and downstream assembly. A single machine speed does not prove finished furniture capacity.
Staffing should be determined from observed tasks including loading unloading inspection replenishment waste handling assembly supervision maintenance and breaks.
Installation commissioning and training
Site planning should verify access foundations floor load clearances layout utilities extraction network data storage climate material routes and maintenance space. Commissioning should test each machine and the complete data and material flow.
Training should cover software order release operation quality changeover tooling adhesives labels recovery maintenance safety and controlled production records.
Maintenance and lifecycle support
Preventive maintenance should cover cutting tools spindles saws guides belts conveyors edge banding units glue systems drills clamps extraction sensors controls scanners printers and safety devices.
Agree approved tooling consumables adhesives edge materials lubricants filters wear parts software backups licenses manuals service responsibility and spare parts before acceptance.
How to select the correct line
Provide product drawings bills of materials annual and shift mix panel types sizes thicknesses finishes hardware batch sizes target quality output changeovers existing machines factory layout utilities staffing and expansion plan.
The technical review should map the route calculate station loads identify bottlenecks define buffers and propose an acceptance trial using representative orders.
Supplied claims requiring evidence
The supplied description mentions an approximate footprint of ten by twenty metres an area near two hundred square metres output of one hundred to one hundred twenty panels in eight hours a stated panel size of twelve hundred twenty by fourteen hundred forty millimetres and five to six workers.
These figures require an approved layout machine list product definition shift assumptions measured cycle study staffing plan and acceptance test. Claims about improved efficiency panel utilization labor saving easy operation or high return also require documented baselines and calculations.
Technical information to verify
Confirm every machine function capacity working range speed tolerance tooling control software interface label method edge system drill data handling equipment extraction utilities dimensions weight foundation safety options and standard scope.
Also verify layout production assumptions staffing service training warranty consumables spare parts acceptance criteria approved image rights and the exact source and date of every published figure.
Limitations and publishing status
The supplied text and image do not verify the exact line composition footprint production rate staffing requirement software performance efficiency savings return on investment or suitability for a specific factory.
Publication requires approved machine datasheets a controlled layout process routing cycle calculation representative trial safety review image approval bilingual technical review staging review and final content approval.
Questions we are asked
What is a cabinet production line?
It is an integrated workflow that converts approved cabinet designs into identified cut edged and bored components ready for hardware fitting and assembly.
How is line output verified?
Use a timed acceptance trial with representative orders stated shifts staffing material supply quality criteria changeovers and downtime rules.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- CNC WOOD ROUTER CNC routing solutions for cutting, drilling, engraving and machining suitable wood panels and furniture components.
- CNC ROUTER WITH ROTARY A CNC router equipped with a rotary attachment or axis for machining suitable cylindrical and shaped workpieces. Selection depends on the part geometry, material, dimensions, required operations, accuracy, and production volume.
- Automatic Edge Banding Machines Automatic edge banding machines apply and finish compatible edge material on straight panel edges through a controlled production sequence. Correct selection depends on the panel material dimensions edge tape adhesive production volume finish requirement installed processing units utilities and extraction system.