

UNIVERSAL MILLING MACHINES
Universal Horizontal Milling Machine with DRO
A universal horizontal milling machine with a digital readout for machining suitable faces, slots, grooves, gears, helical features, and other accessible workshop components. The correct model depends on workpiece size, material, table movement, swivel requirements, spindle, arbor tooling, tolerance, finish, and production pattern
A universal horizontal milling machine uses a horizontal spindle and arbor arrangement to carry suitable milling cutters. The table normally provides longitudinal, cross, and vertical positioning, while a verified universal table may swivel to support selected angular or helical machining setups. The digital readout displays axis position from installed scales and can help the operator set datums and monitor movement. DRO resolution does not equal finished machining accuracy, which also depends on machine geometry, backlash, setup, tooling, cutting forces, thermal behavior, and inspection.
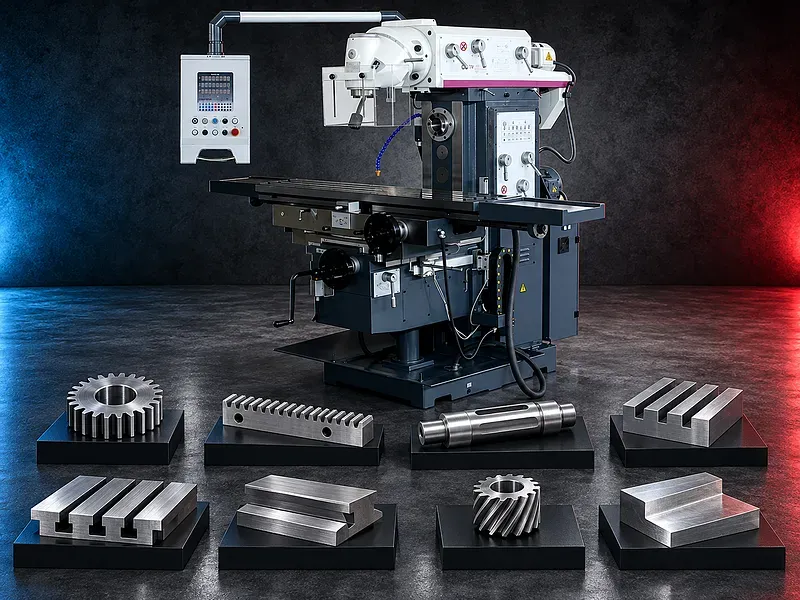
Universal horizontal milling concept
The horizontal spindle drives cutters mounted directly or on an arbor supported by the overarm and arbor support according to the machine design. The table positions the workpiece relative to the rotating cutter.
The universal designation commonly refers to additional table swivel or accessory capability, but the exact swivel arrangement, angle range, gear train, dividing functions, and supported operations require model verification.
Potential milling operations
Potential operations include slab milling, face milling, side milling, slotting, keyway cutting, straddle milling, gang milling, angular milling, form milling, gear cutting, and selected helical work when supported by the machine, accessories, tooling, and setup.
Vertical milling, drilling, boring, or other operations may require a verified vertical head or additional attachment and must not be assumed from the horizontal machine name alone.
Universal table and angular work
A verified swiveling table may allow the workpiece feed direction to be set at an angle relative to the spindle. With suitable gearing, indexing, and accessories, selected helical or spiral features may be possible.
Swivel range, angle setting method, table locking, graduation accuracy, lead range, change gears, indexing head compatibility, and supported helical operations are model and accessory specific.
Horizontal spindle arbor and support
The spindle and arbor system carry slab, side, face, form, and other compatible cutters. Arbor diameter, spindle taper, spacers, keys, cutter width, overarm position, and arbor support must match the operation.
Excessive arbor overhang, weak support, incorrect spacers, poor alignment, worn bearings, or unbalanced cutters can cause vibration, poor finish, dimensional error, or safety risk.
Digital readout system
A verified DRO may display longitudinal, cross, and vertical axis positions and provide functions such as datum setting, zeroing, coordinate display, and selected calculation support depending on the installed unit.
The exact number of displayed axes, scale type, resolution, accuracy, compensation functions, protection, installation, and calibration require verification. The DRO does not correct mechanical wear or poor setup.
Suitable workpieces and applications
Potential workpieces include machine bases, plates, blocks, brackets, fixtures, shafts, gear blanks, slide components, tooling parts, maintenance components, and other parts suited to horizontal cutter access.
Potential applications include maintenance workshops, toolrooms, repair production, machine building, training workshops, prototypes, individual parts, and small or medium batches requiring flexible conventional machining.
Workpiece materials
Potential materials may include suitable grades of steel, cast iron, aluminum, copper alloys, and other machinable materials compatible with the verified spindle, cutter, rigidity, power, speed, feed, and coolant system.
Material grade, hardness, casting skin, scale, welded areas, interrupted cuts, inclusions, heat treatment, stock allowance, and required finish must be reviewed before confirming the process.
Tooling accessories and workholding
Potential tooling includes slab mills, side and face cutters, slotting cutters, angle cutters, form cutters, gear cutters, arbors, sleeves, spacers, holders, and adapters compatible with the spindle and arbor system.
Workholding and accessories may include vises, clamps, angle plates, rotary tables, dividing heads, tailstocks, change gears, fixtures, parallels, supports, and a vertical head where verified and required.
Table movement feeds and setup
The table, saddle, and knee provide longitudinal, cross, and vertical positioning. Powered feeds or rapid movement may be available on selected axes according to the verified machine.
Setup should control table load, overhang, travel, backlash, locks, cutter access, arbor clearance, support position, cutting direction, climb or conventional milling strategy, chip flow, coolant, datum transfer, and inspection access.
Speeds feeds and cutting strategy
Spindle speed, table feed, depth and width of cut, cutter engagement, coolant, and pass sequence should suit the material, cutter, machine rigidity, available power, finish, and tool manufacturer recommendations.
Roughing and finishing may require different cutters and settings. Excessive cutting load, poor arbor support, weak workholding, or trapped chips can reduce tool life, finish, accuracy, and safety.
Accuracy and inspection
The acceptance plan may include dimensions, flatness, straightness, parallelism, perpendicularity, slot width and depth, angular features, gear or helix characteristics, surface finish, and fit with mating parts.
Finished quality depends on machine geometry, guide condition, backlash, spindle and arbor runout, support alignment, thermal behavior, workholding, cutter condition, cutting data, datum strategy, and calibrated inspection equipment.
How to choose the correct machine
Provide component drawings with material, hardness, dimensions, weight, features, maximum machining envelope, angles, helical or gear requirements, tolerances, finish, quantities, batch sizes, setup constraints, and current production route.
Selection should also consider table dimensions, table load, longitudinal cross and vertical travels, table swivel, spindle taper, speed range, feeds, rapid movement, motor power, arbor sizes, overarm support, DRO axes, attachments, coolant, tooling, and floor space.
Technical information to verify
The approved exact model source must confirm the manufacturer, brand, model, machine type, table dimensions, table load, longitudinal travel, cross travel, vertical travel, table swivel range, spindle taper, spindle speed range, table feeds, rapid movement, and motor power.
It must also confirm arbor dimensions, overarm and support, positioning accuracy, repeatability, DRO axes and resolution, guideway type, lubrication, coolant, electrical supply, dimensions, weight, foundation, included cutters and accessories, guards, and safety devices.
Coolant chips and maintenance
Suitable coolant may control heat, lubricate the cut, support cutter life, and carry chips when required by the material and tooling. Chips should be controlled around the cutter, arbor, support, workpiece, vise, table, T slots, guards, and guide surfaces.
Preventive maintenance should cover lubrication, spindle bearings, arbors, overarm support, gears, feeds, screws, nuts, gibs, guideways, axis locks, DRO scales, coolant, electrical controls, guards, and periodic geometry checks.
Safety requirements
The risk assessment should address rotating cutters, arbors, spindles, exposed keys, entanglement, sharp and hot chips, cutter breakage, ejected workpieces, heavy lifting, clamping, axis movement, pinch points, coolant, and electrical hazards.
The exact guards, emergency stops, spindle cutter and arbor checks, workholding procedures, safe setup zones, lifting plan, operating instructions, training, personal protective equipment, and maintenance controls must follow approved documentation and site requirements.
Installation and lifecycle support
Site planning should cover machine footprint, foundation, leveling, lifting access, workpiece route, electrical supply, grounding, coolant, lubrication, chip collection, lighting, ventilation, tooling storage, inspection space, maintenance access, and operator training.
The exact supply scope, commissioning, training, preventive maintenance, spindle arbor support and guideway service, DRO calibration, consumables, spare parts, warranty, and service commitments require confirmation in the approved technical and commercial offer.
Limitations and alternative processes
A universal horizontal milling machine with DRO is not automatically suitable for every workpiece, material, size, weight, geometry, tolerance, finish, batch volume, or productivity target.
A vertical mill, turret mill, bed type mill, CNC machining center, gear hobbing machine, broaching machine, grinder, or another process may be more suitable for some applications.
Technical review and next step
Send the component drawings with material, hardness, dimensions, weight, machining features, angular helical or gear requirements, tolerances, finish, quantities, setup constraints, available tooling, and target output.
SAKKARY MACHINERY will review the machining envelope, table spindle and arbor requirements, DRO, accessories, workholding, process sequence, inspection, utilities, safety needs, alternative processes, and information that still requires manufacturer verification.
Questions we are asked
What is a universal horizontal milling machine?
It is a milling machine with a horizontal spindle and a table or accessory arrangement that may support selected angular helical or dividing work in addition to standard horizontal milling.
What does the DRO do?
The digital readout displays axis position from installed scales and helps with datum setting and movement monitoring but it does not guarantee finished machining accuracy.
Which operations can the machine perform?
Potential operations include slab side face slot keyway straddle gang angular form and gear milling with selected helical work when supported by the machine and accessories.
Can the machine perform vertical milling?
Only when the exact machine has a verified compatible vertical head or attachment. This capability should not be assumed from the horizontal machine name.
Which workpieces are suitable?
Potential workpieces include bases plates blocks brackets shafts gear blanks fixtures tooling and maintenance parts within the verified table load travels and cutter access.
What information is required for selection?
Provide drawings material hardness dimensions weight features angles helical or gear needs tolerances finish quantities setup constraints and target output.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- Heavy-Duty Gap-Bed Conventional Lathes Heavy-duty conventional lathes for turning large-diameter, long, and heavy rotational components. The gap-bed design provides additional swing near the headstock for suitable short workpieces.
- Gantry Type Milling Machine A gantry-type milling machine provides an open working area for machining suitable large or heavy components. Selection depends on workpiece dimensions, weight, material, required operations, tolerances, finish, and production requirements.
- Boring Machine for Workshop Machining A boring machine for drilling, enlarging, finishing, and aligning suitable holes in individual parts and small production batches. The correct model depends on workpiece size, material, hole diameter, depth, tolerance, surface finish, setup, tooling, and required output.