

ROUND DUCT BEADING AND EDGE FORMING
Round Duct Grooving and Beading Machine
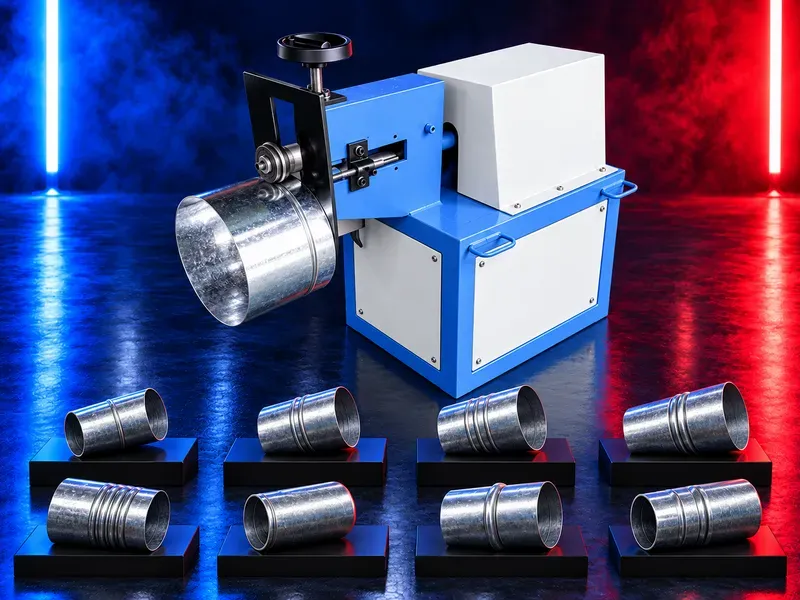
A round duct grooving machine uses matched forming rollers to create beads grooves or approved edge profiles on round ducts and fittings. Manual and electric variants serve different workloads while suitability depends on duct diameter material thickness required profile roller design support method and production volume.
The operator positions a prepared round duct or fitting between matched rollers and controls engagement while the workpiece rotates. The roller profile and setting determine the shape depth and location of the formed feature. Standard or special rollers may support beading grooving flanging or other approved forms. Every profile requires a drawing compatible tooling and a sample trial rather than a general capability claim. Claims for manual and electric availability broad application custom profiles or seamless integration with a complete round duct line require confirmation from the exact configuration and approved technical documentation.
What the machine does
The machine plastically forms a local profile around the circumference of a round duct or fitting using matched rollers. Depending on verified tooling the result may be a reinforcing bead groove edge flange or another defined form.
It does not replace cutting rolling seam forming or seam closing operations unless these are included in a separate approved configuration.
Manual and electric variants
A manual drive can suit occasional work smaller parts or site tasks where the verified force and operator effort are acceptable. An electric drive can provide more consistent rotation for repeated production.
Compare actual size range workload utilities control and safety rather than selecting by drive type alone.
Profile drawing and purpose
Provide a cross section drawing with profile shape depth width radius location and tolerance. Define whether the feature is for stiffness connection retention sealing clearance or appearance.
Terms such as flange envelope mortise and bead groove can be interpreted differently and must be supported by a drawing.
Roller tooling
Upper and lower rollers must form a matched set for the specified profile material and thickness. Incorrect rollers or clearance can distort the duct mark the surface or create cracks.
Confirm roller identification dimensions material hardness mounting adjustment wear limits storage and safe changeover.
Workpiece requirements
Specify duct or fitting diameter length material grade thickness seam type roundness surface condition and end preparation. The forming location must remain accessible to both rollers and supports.
Beads seams fittings branches or existing flanges may restrict tool access and should be reviewed on representative parts.
Forming cycle and adjustment
The workpiece rotates while the rollers engage progressively until the specified profile is reached. Feed pressure gap and number of passes should avoid sudden deformation and uncontrolled springback.
Record approved setup references for every material size and profile combination.
Support and positioning
The round section should be supported at the machine working height without sagging flattening or side load. Long large or flexible parts may require adjustable stands or assisted rotation.
Confirm reference location forming distance from the end operator reach loading direction and discharge clearance.
Materials and thickness
Material grade coating thickness hardness temper and surface finish influence force springback marking cracks and roller wear. Galvanized steel stainless steel aluminium and other materials require separate confirmation.
Do not generalize the same diameter or thickness range across profiles materials or drive variants.
Quality control
Inspect profile shape depth width location continuity roundness end condition seam integrity surface marking cracks coating damage and fit with the next assembly operation.
Approve the first part after setup roller change material batch change adjustment maintenance or extended stoppage.
Flanging and special forms
A flange or special shape can only be claimed when dedicated rollers machine clearance force and process trials are approved for that geometry. Some end connections may be better served by a dedicated flange rolling machine.
Compare profile quality changeover and total workflow before combining unrelated operations on one machine.
Integration in round duct production
The grooving station may follow sheet cutting rolling lock forming and seam closing. End flanging fitting assembly sealing inspection and installation preparation may follow.
Coordinate diameter length seam orientation profile location and handling with every upstream and downstream machine.
Productivity and labor
Accepted output depends on diameter profile depth material handling number of passes drive type setup inspection and surrounding process capacity.
Measure accepted parts per shift and changeover time during representative trials instead of relying on general efficiency claims.
Common process risks
Wrong rollers excessive engagement poor support incorrect reference worn tooling uneven rotation or unsuitable material can cause variable profiles flattening wobble scratches cracks coating damage or seam opening.
Stop production and correct tooling support material or settings when the result falls outside acceptance criteria.
Safety and operator protection
The machine contains rotating rollers in running nip points sharp sheet edges and powered movement in electric versions. Guards protected controls emergency stops and energy isolation must follow the approved risk assessment.
Procedures must cover loading support hand position trial forming unloading jams roller changes cleaning and maintenance.
Installation and site readiness
Confirm stable level placement electrical supply for powered versions working clearance full workpiece rotation support stands lighting noise control material routes and maintenance access.
Portable or site use requires an approved transport method secure positioning cable protection and suitable environmental conditions.
Training maintenance and lifecycle support
Training should cover profile drawings roller identification setup references work support controls quality checks safe recovery isolation and daily inspection.
Preventive maintenance should address shafts bearings gears drive components rollers guides adjustment screws guards electrical connections lubrication fasteners and emergency devices. Prepare approved rollers wear parts and spares.
How to select the correct machine
Start with profile drawings round duct and fitting diameters materials thickness length range seam types quantities utilities floor plan handling method and changeover needs.
Selection should confirm manual or electric drive roller sets forming force clearance supports speed control guarding maintenance service support and representative trials.
Technical information requiring verification
Verify available drive types compatible profiles diameter and length ranges materials thickness range roller dimensions forming force speed motor power electrical data controls accuracy noise dimensions and total weight.
Confirm special roller capability supports guards portability standards installation commissioning training warranty service scope spare parts and acceptance tests from approved documentation.
Publishing status
This page describes the machine category forming process and selection logic. Exact profiles sizes thickness power speed capacity tooling utilities standards and commercial commitments require an approved data sheet roller drawings and technical review before publication.
Questions we are asked
What is a round duct grooving machine?
It uses matched rollers to form a bead groove or approved edge profile around a round duct or fitting.
What is the difference between manual and electric types?
Manual machines depend on operator drive while electric machines provide powered rotation. Verified capacity controls workload and safety determine suitability.
Can it create every flange or special shape?
No. Each profile requires compatible rollers clearance force settings and a representative approved trial.
Does beading make every duct stronger?
A bead may improve stiffness when correctly designed but structural performance depends on duct size material thickness profile geometry and support design.
How is forming quality checked?
Check profile shape depth width location continuity roundness surface condition seam integrity and fit with the next operation.
What information is needed for selection?
Provide profile drawings duct diameters materials thickness lengths seam types quantities utilities layout and representative parts.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- Spiral Duct Forming Machine A forming machine for producing round spiral air ducts from compatible metal strip. Machine selection depends on duct diameter, material, strip thickness and width, seam type, cut length, and production target.
- U Shape Automatic Duct Production Line A U shape automatic duct production line converts approved sheet metal coils into prepared duct sections through a coordinated sequence that may include uncoiling leveling beading punching shearing locking flange forming and folding. The correct configuration depends on duct type material thickness dimensions flange system output target and factory layout.
- Automatic Duct Production Line for Rectangular HVAC Ducts An automatic duct production line converts approved sheet metal coils into prepared rectangular HVAC duct blanks and folded sections through a coordinated linear workflow. Depending on the verified configuration it may integrate uncoiling leveling beading punching shearing transfer locking flange forming and folding