

RECTANGULAR DUCT SEAM CLOSING
Hydraulic Lock Seam Closing Machine for HVAC Ducts
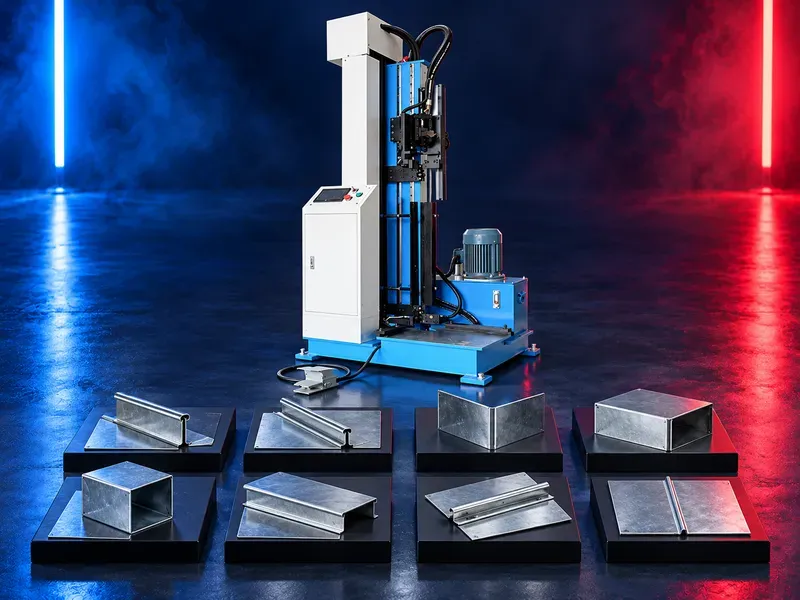
A hydraulic lock seam closing machine closes a prepared longitudinal seam on rectangular HVAC duct sections using controlled hydraulic force and guided tooling. Correct selection depends on seam profile sheet material thickness duct length section geometry required tightness and production workflow.
The operator places the preformed mating seam into the closing area and supports the duct section against the machine reference. The hydraulic cycle drives the closing tool along or against the seam according to the supplied design until the approved joint is completed. A programmable controller may manage clamping closing return and cycle interlocks. The actual sequence tooling and level of automation must match the lock profile produced by the upstream forming machine. Claims for thickness range maximum duct length tight smooth fast and safe sealing require confirmation from the exact machine data sheet representative duct trials and approved acceptance criteria.
What the machine does
The machine closes a compatible longitudinal lock seam after the sheet edges have been formed and engaged. Hydraulic force completes the joint in a controlled cycle for later sealing inspection and duct installation.
The result depends on seam geometry engagement alignment support tooling condition hydraulic settings and inspection.
Prepared lock seam
Both mating seam profiles must be formed to the approved dimensions before closing. Incorrect allowances damaged edges or incomplete engagement can prevent uniform closure.
Confirm the seam type orientation overlap and compatibility with the installed closing tool before production.
Hydraulic closing cycle
The hydraulic system generates the force required to press or travel the closing tool through the seam. Pressure flow and motion should be controlled to close the joint without crushing the duct panel.
Verify approach closing dwell return and release stages and define the approved settings for each material and seam profile.
Programmable cycle control
A programmable controller may sequence clamps valves motion and safety interlocks and store approved operating parameters. Clear controls reduce variation between operators.
Confirm available recipes sensors diagnostics access levels reset behavior backup and safe recovery after interruption.
Closing tool and guides
The closing tool must match the seam profile and guide the joint without opening twisting or marking it. Tool straightness contact geometry and wear influence the finished seam.
Verify tool material replacement method adjustment wear limit lubrication and availability of tooling for additional seam types.
Duct support and positioning
The duct section should be supported along its length and held square to the closing path. Large flexible or thin panels may need adjustable stands or additional operator support.
Confirm minimum and maximum duct dimensions support height reference stops and handling method for completed sections.
Materials and thickness
Provide sheet grade coating thickness hardness and surface finish together with the formed seam drawing. Galvanized sheet stainless steel aluminium or other materials require separate force tooling and sample confirmation.
The thickness range must be verified for the exact seam and duct geometry because one value cannot represent every material.
Duct length and section geometry
The usable closing length and machine clearance must accommodate the full seam and duct cross section. Flanges bends reinforcement and large panels can affect access and support.
Review the largest and smallest representative ducts including transitions offsets and special sections before selection.
Seam tightness and sealing
Mechanical closing creates the joint shape but does not by itself guarantee the required leakage class. Sealant gasket preparation and workmanship may also be required by the duct standard.
Define visual dimensional and leakage related acceptance criteria and the sealing process before production release.
Hydraulic pneumatic and electric alternatives
Lock seam closing machines may use hydraulic pneumatic or electric actuation. The suitable option depends on seam load production volume controls utilities portability maintenance skills and site conditions.
Compare closing force cycle consistency energy source noise service needs and integration rather than selecting by drive name alone.
Integration in duct production
The machine normally follows cutting beading notching TDF flange forming folding and lock forming operations. Clip cutting corner fitting and sealing may continue after closing.
Coordinate blank allowances seam orientation and handling so the prepared section reaches the closer without damage or reversal errors.
Productivity and labor
Output depends on duct size thickness seam length loading support cycle settings unloading inspection and the capacity of surrounding operations.
Measure accepted closed ducts per shift during representative trials instead of relying on general speed or labor saving claims.
Quality control
Acceptance should cover seam closure straightness continuity surface marking panel distortion end condition corner fit and compatibility with sealing and installation.
Inspect the first section after tooling adjustment material change hydraulic setting change or maintenance using approved gauges and test methods.
Common process risks
Incorrect seam formation poor engagement inadequate support excessive pressure worn tooling or misalignment can cause open sections crushing waviness scratches twist or leakage paths.
Stop and correct upstream forming and closing settings when the seam falls outside acceptance criteria.
Safety and operator protection
The machine contains hydraulic force moving tools clamps pinch points stored pressure and sharp sheet edges. Guards interlocks emergency stops pressure isolation and controlled access should follow the approved risk assessment.
Safe procedures must cover loading support engagement trial cycles unloading jam recovery pressure release cleaning tooling work and maintenance.
Installation and site readiness
Site preparation should confirm level foundation electrical supply hydraulic oil cooling required compressed air working clearance duct supports lighting and service access.
Provide safe routes for unfinished and closed duct sections and enough space to prevent panels from striking people or equipment.
Training maintenance and lifecycle support
Training should cover seam identification engagement support recipes hydraulic settings quality checks safe recovery pressure isolation and daily inspection.
Preventive maintenance should address oil quality filters cylinders seals valves hoses guides tools sensors guards clamps electrical controls and emergency devices. Prepare approved spare parts and consumables.
How to select the correct machine
Start with seam drawings duct materials thickness range closing length minimum and maximum section sizes product mix shift target leakage requirement supports utilities and site layout.
Selection should confirm actuation type tooling force cycle control clearance handling integration service support and representative closing trials.
Technical information requiring verification
Verify compatible seam profiles material types thickness range maximum closing length section clearance hydraulic force pressure travel speed cycle time tooling controls accuracy oil capacity cooling electrical load compressed air dimensions foundation load and total weight.
Confirm supports guards leakage test basis installation commissioning training warranty service scope spare tooling parts and acceptance tests from approved documentation.
Publishing status
This page describes the machine category process and selection logic. Exact thickness length force speed output leakage performance materials controls options standards and commercial commitments require an approved data sheet and technical review before publication.
Questions we are asked
What is a hydraulic lock seam closing machine?
It is a machine that uses controlled hydraulic force and matched tooling to close a prepared longitudinal seam on rectangular HVAC duct sections.
Which seam profiles can it close?
Compatibility depends on the installed closing tool and the mating profile produced upstream and must be confirmed from drawings and trials.
Does closing the seam guarantee no leakage?
No. Leakage performance also depends on seam preparation sealant gasket corners workmanship and the applicable duct standard.
What is the difference between hydraulic pneumatic and electric closing?
The actuation method changes available force cycle behavior utilities maintenance and portability. The correct choice depends on the production requirement.
How is seam quality checked?
Check complete closure straightness continuity panel distortion surface condition end details corner fit and any required leakage test.
What information is needed for selection?
Provide seam drawing material thickness duct length section dimensions quantities leakage requirement support method utilities and factory layout.
Tell us the part you need to make
An engineer reads every request. Usually the same working day.
Related
- Spiral Duct Forming Machine A forming machine for producing round spiral air ducts from compatible metal strip. Machine selection depends on duct diameter, material, strip thickness and width, seam type, cut length, and production target.
- U Shape Automatic Duct Production Line A U shape automatic duct production line converts approved sheet metal coils into prepared duct sections through a coordinated sequence that may include uncoiling leveling beading punching shearing locking flange forming and folding. The correct configuration depends on duct type material thickness dimensions flange system output target and factory layout.
- Automatic Duct Production Line for Rectangular HVAC Ducts An automatic duct production line converts approved sheet metal coils into prepared rectangular HVAC duct blanks and folded sections through a coordinated linear workflow. Depending on the verified configuration it may integrate uncoiling leveling beading punching shearing transfer locking flange forming and folding