Short Answer
Wire EDM cuts through-profiles in conductive materials using wire, while sinker EDM forms cavities and internal shapes using an electrode. Choose by geometry, accuracy, finish, cycle time and consumables.
Start with geometry
If the path is through-cut and wire can pass, wire EDM is a strong candidate. Blind cavities and electrode-transferred shapes usually point to sinker EDM.
Material and preparation
Both require conductive material. Review heat treatment, start holes, workholding, surface condition and electrode manufacture where applicable.
Accuracy and finish
Define tolerance, roughness, acceptable passes and thermal-fluid stability. Unneeded precision adds time and cost.
Operating cost
Include wire or electrode, filters, dielectric, power, programming, supervision and maintenance, then compare cost per good part.
Frequently Asked Questions
Can EDM machine non-conductive materials?
Not in conventional use; the process relies on electrical conductivity.
Which is more accurate?
It depends on the application, machine and setup; there is no universal answer.
Why does the electrode matter?
Its geometry, material, manufacture and wear directly affect sinker EDM results.
Next Step
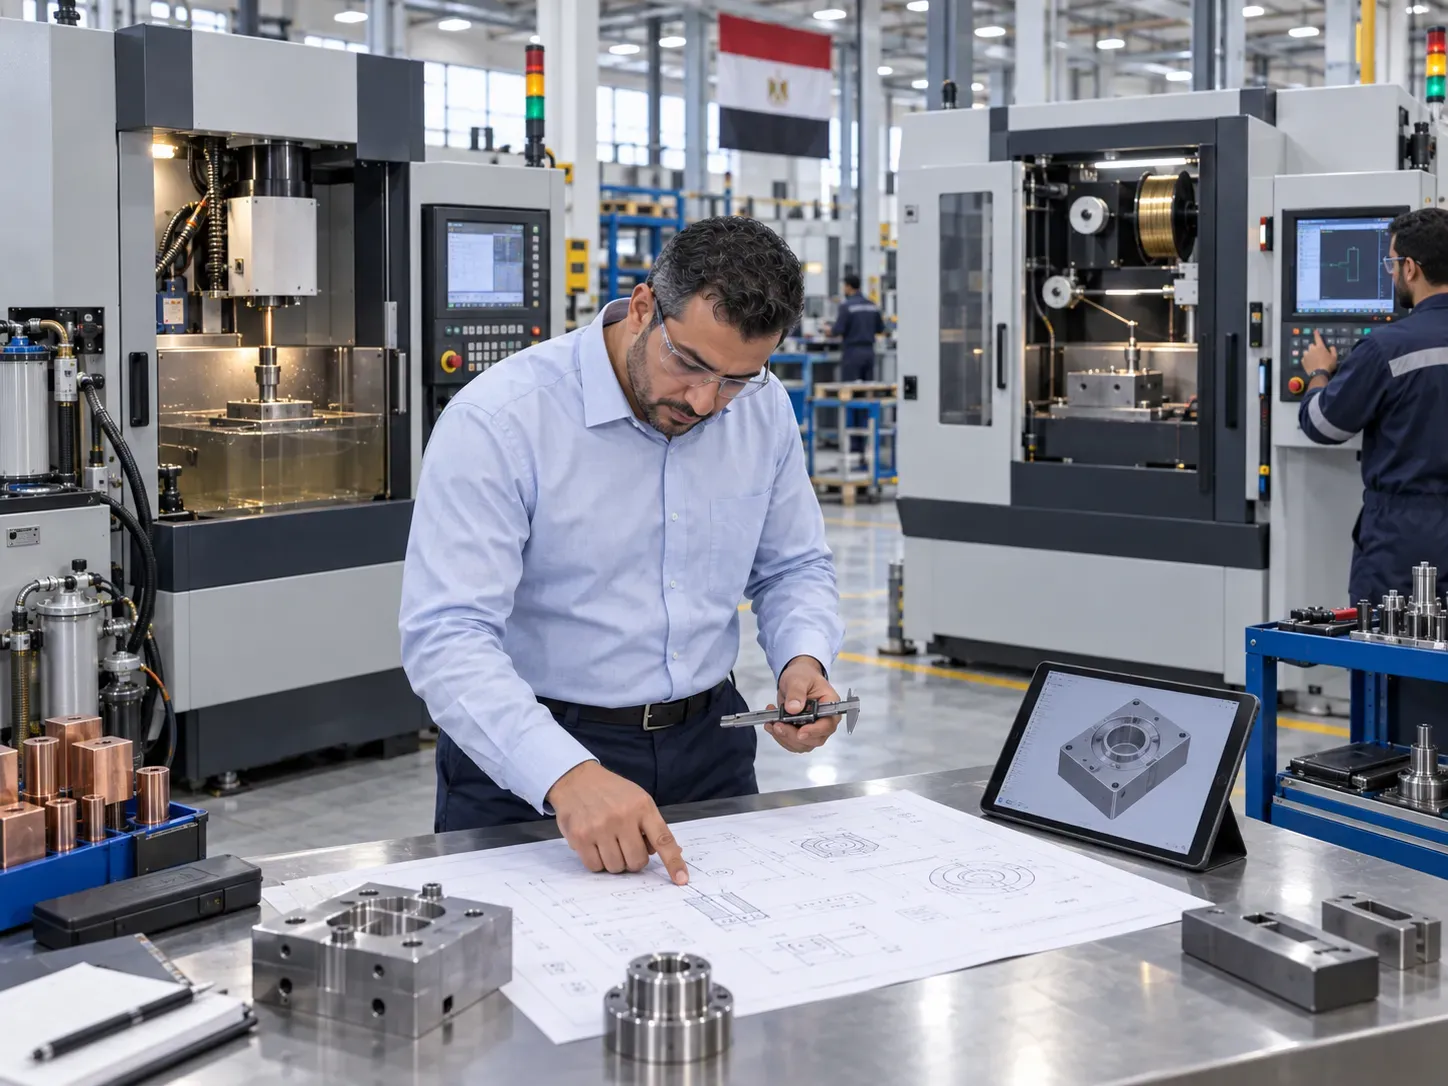
Share the part drawing, material, tolerance and finish to determine the suitable EDM route.
Need a machine, tooling or a service visit?
Request a price