How to Retain Machine Operator Skills After Training: A Practical Follow-Up Plan
8 min read
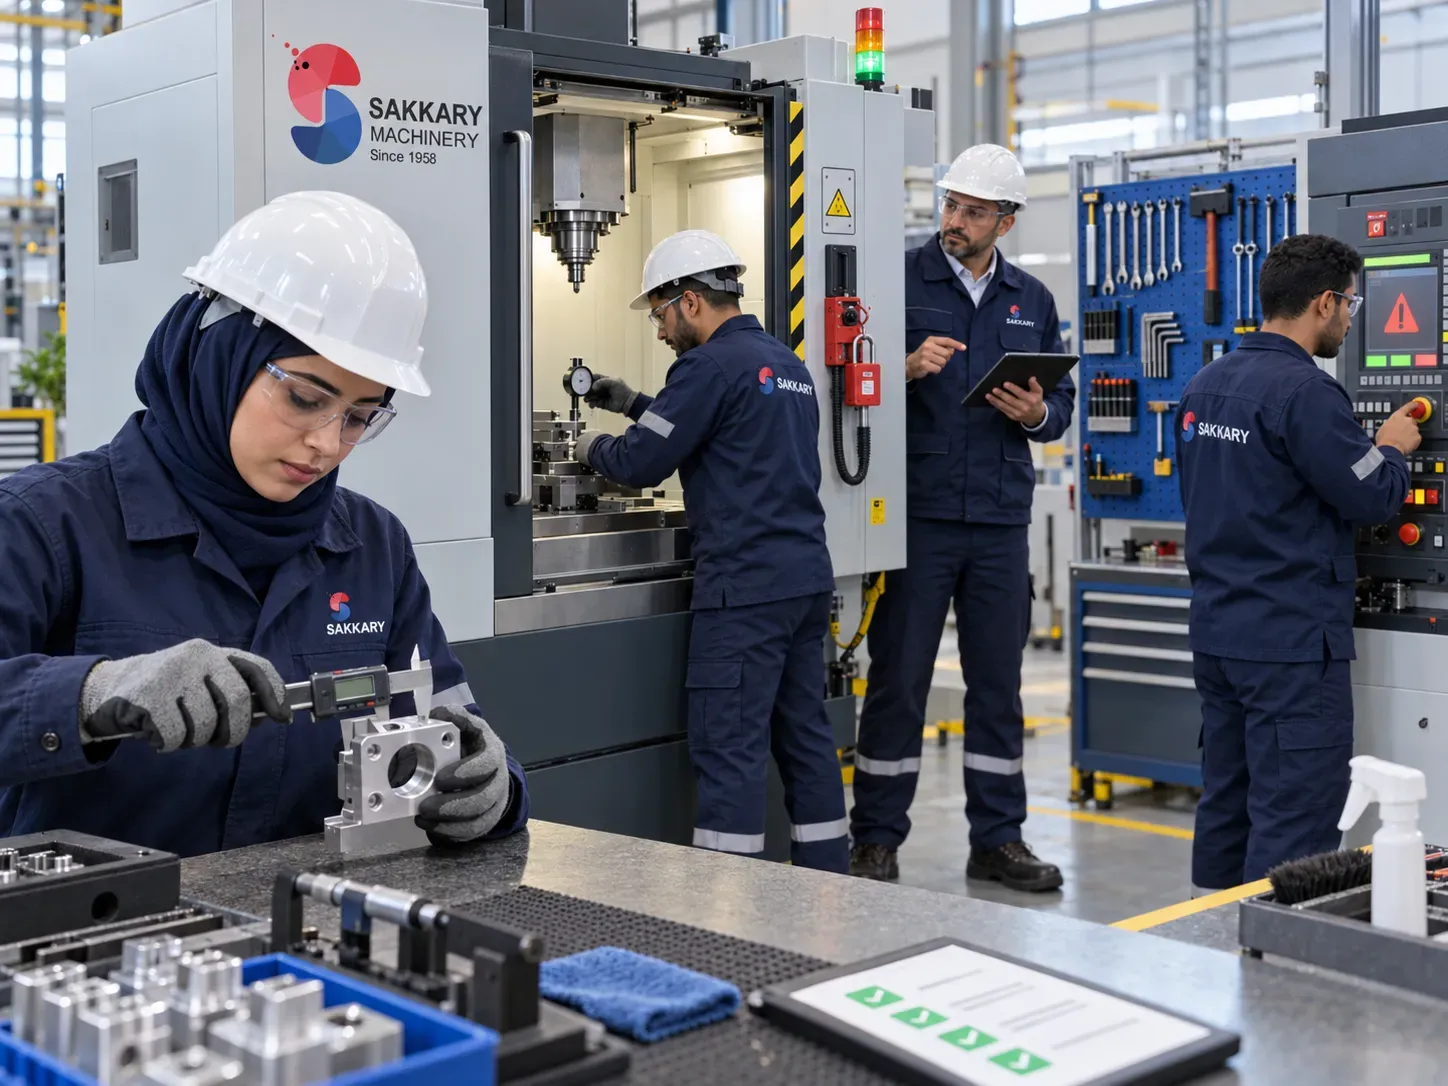
Training is not complete when the instructor leaves the factory. It is complete only when the required work can be performed correctly, consistently and within the operator's approved authority under normal production conditions. A good course may introduce a method and correct misunderstandings, but competence can still decline if the skill is not practised, if standards are unclear, or if a process change reaches the shop floor without an accompanying review.
Retaining skills therefore requires a simple operating system: define the critical tasks, observe them at work, record evidence, correct gaps early and reassess whenever the job changes. The objective is not to turn every shift into a classroom. It is to make correct practice visible, repeatable and transferable between people and shifts.
Why operator skills decline after training
Skill loss is not always a memory problem. It often begins with the production environment. An operator may have attended a useful session but then return to a machine that is unavailable, a different product, an outdated work instruction or a shift where an experienced colleague informally teaches a different method.
Common causes include:
- A trained task is rarely performed, so the operator has little opportunity to practise it.
- The machine, control, tooling, material, drawing or production sequence changes.
- The documented standard is missing, difficult to access or inconsistent with actual practice.
- Production pressure encourages shortcuts or dependence on one experienced person.
- Supervisors check output quantity but do not observe the critical steps that influence safety and quality.
- Operators move between machines or return after a long absence.
- An assessment records attendance rather than demonstrated performance.
- Shift handovers do not carry forward relevant settings, tool status, alarms or quality notes.
The response should match the cause. Repeating the entire original course is not always the answer. A narrow gap may need supervised practice and a short reassessment. A changed process may require an updated instruction and change-specific training. A repeated error across several shifts may indicate a system issue rather than an individual failure.
Start with a task-based definition of competence
Avoid labels such as “good operator” or “knows the machine.” They are too broad to assess and too vague to improve. Break each role into observable tasks based on the approved machine documentation, workplace procedures and the operator's actual responsibilities.
Depending on the machine and application, a role may include:
- Recognising applicable hazards, guards, warnings and escalation points.
- Completing approved pre-use checks and confirming that the work area is ready.
- Identifying the correct job documentation, material, tooling and measuring equipment.
- Following the approved start, production, inspection and shutdown sequence.
- Loading or selecting an approved program without changing protected parameters.
- Producing or supporting the first-piece verification according to the factory's procedure.
- Recording measurements, defects, downtime or abnormalities in the required record.
- Performing the permitted daily care tasks and escalating work that belongs to maintenance.
- Responding to an alarm within the operator's defined authority, without bypassing safeguards.
- Handing over the machine and job status clearly to the next shift.
Not every operator needs the same level for every task. Define the required level for each role and shift before assessing anyone.
Build a skills matrix that supports decisions
A skills matrix should show more than names and course dates. It should connect people to machines or processes, required tasks, current demonstrated level, evidence date and the next required action.
A practical four-level structure can be:
- Introduced: has received an explanation or demonstration but is not authorised to work independently.
- Performs under supervision: can complete the task with an approved supervisor or competent colleague present.
- 7Performs independently: has demonstrated the task to the agreed standard and is authorised for the defined scope.
- Approved internal coach: can perform the task and support others using the approved method, subject to the factory's authorisation rules.
The matrix should also state the scope. Competence on one machine, controller, material family or operation does not automatically prove competence on another. Include an evidence reference such as an observation record, practical test, approved sample or supervisor sign-off. Set a review trigger rather than assuming a certificate remains current forever.
Use the matrix to answer operational questions:
Does every shift have adequate coverage?
Which task depends on one person?
Who needs supervised practice before a new job starts?
Where is refresher training a priority?
A matrix that does not influence these decisions quickly becomes an administrative file.
Create a follow-up cycle after initial training
The follow-up plan should be agreed before the course closes. The actual frequency must reflect risk, task complexity, production pattern, legal requirements, manufacturer guidance and internal policy; it should not be copied from a generic interval.
1. Confirm immediate workplace application
Identify when the trainee will next perform the relevant task and who will supervise the first applications. Make sure the correct instruction, drawing, checklist and measuring tools are available. If the production task differs materially from the training example, record the difference and decide whether additional guidance is required.
2. Observe real performance
Use a task-specific checklist while the operator completes normal work. Observe the sequence, decisions, records and escalation behaviour, not only the final part. The assessor should avoid coaching during a formal assessment unless an intervention is needed to prevent harm; assistance should be recorded because it affects the result.
3. Give specific feedback
Feedback should describe the observed step, the required standard and the action needed. “Be more careful” is not a corrective action. A useful note might identify that the operator used the right inspection tool but did not record the result in the required location. This makes the follow-up measurable.
4. Assign a targeted response
Choose the smallest adequate intervention: repeat a demonstration, arrange supervised practice, clarify a work instruction, correct an unavailable tool, provide a focused refresher, or suspend independent performance of a task until reassessment. Do not use training to conceal an equipment, documentation or management problem.
5. Reassess and close the gap
Record whether the operator can now demonstrate the task without unplanned assistance. If not, document the remaining gap, temporary controls, responsible person and next review. Closure means demonstrated performance, not merely attendance at another session.
Use short refreshers for specific gaps
Refresher training is strongest when it is linked to evidence. It can focus on one recurring mistake, one inspection step, one change in the production method or one handover weakness. The content should state what changed, what the operator must do, what is outside the operator's authority and how competence will be checked.
Useful formats may include a toolbox briefing, supervised practice on an approved task, a guided review of a work instruction, a controlled simulation, or a practical reassessment. The format depends on the risk and the nature of the skill. A verbal reminder alone is not sufficient evidence for a safety-critical or quality-critical task unless the applicable approved procedure specifically accepts it.
Do not turn refresher training into a list of unsafe troubleshooting tips. Machine-specific actions must follow the manufacturer's instructions and the factory's approved procedures. Operators should never be encouraged to bypass guards, override interlocks, enter protected areas, alter protected parameters or perform electrical or maintenance work outside their authorisation.
Reassess after change, absence or abnormal events
Calendar-based reviews alone are not enough. Add event-based triggers. A competence review may be needed after:
- A new machine, control, software version or production method is introduced.
- Tooling, material, drawing, specification or inspection requirements change.
- An operator transfers roles or returns after extended absence.
- A defect, near miss, repeated alarm or procedural deviation indicates a possible skill gap.
- A work instruction or safety control is revised.
- The operator has not performed a critical task for a significant period defined by the factory.
- An audit shows that documented and actual practice differ.
The review does not automatically mean retraining from the beginning. First determine what changed and which tasks are affected. Then confirm the appropriate technical source, revise controlled documents where necessary and assess only the relevant competence unless broader evidence suggests otherwise.
Frequently asked questions
How often should machine operators receive refresher training?
There is no responsible universal interval for every machine and task. Set the review based on risk, complexity, frequency of use, performance evidence, manufacturer information, legal requirements and internal policy. Use change, absence and incident triggers in addition to planned reviews.
Is a training certificate enough to prove competence?
No. A certificate may prove participation or completion of a course. Competence should be supported by practical evidence against a defined task and standard, and authorisation should follow the factory's approved process.
Should every operator be trained on every machine?
Not necessarily. Coverage should match the production plan, shift needs, risk and business continuity requirements. Broad cross-training without adequate practice can create superficial knowledge. Prioritise critical tasks and build depth progressively.
What if the same error returns after refresher training?
Recheck the root cause. The instruction may be unclear, the measuring equipment unavailable, the process unstable, the workload unrealistic or the machine condition unsuitable. More training will not correct a non-training cause.
Can an experienced operator train colleagues?
Experience is valuable but does not automatically qualify someone to assess or train others. An internal coach should demonstrate the approved method, communicate clearly, respect limits of authority and be formally accepted for that role under the factory's system.
Turn training into stable production practice
SAKKARY MACHINERY approaches operator development as part of the production lifecycle, not as an isolated classroom event. The appropriate scope depends on the machine, control, application, operator role and available technical documentation. No machine-specific suitability, duration or performance result should be assumed before these inputs are reviewed.
Need a machine, tooling or a service visit?
Request a price